





-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

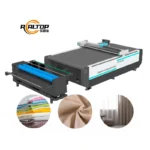
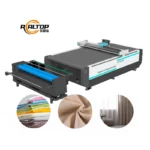
In-house frame and motion engineering — thick-walled seamless steel construction finished on our CNC machining center ensures long-term geometric accuracy across the 1600×2500mm working envelope.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600×2500 mm |
| Machine Size | 3450×2300×1250 mm |
| Rated Power | 9 kW |
| Vacuum Pump | 7.5 kW |
| Table Type | Flat working table with vacuum adsorption |
| Translational Velocity | 800–1200 mm/s |
| Cutting Thickness | 20–80 mm (varies by material type and density — basis to be confirmed) |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor Brand | Delta |
| Guide Rail | iwin rail |
| Frame Construction | Thick-walled seamless steel, high-temperature tempering, CNC machining center finished |
| Vacuum Table Material | Magnesium-aluminum alloy with fluorocarbon PVDF powder spraying, anodic oxidation, hard oxidation |
| Instruction System | HP-GL compatible format |
| Voltage | 380V±10% |
| Safety Device | Infrared sensors, anti-collision, emergency stop |
| Visual Positioning Options | Small CCD camera mark point positioning, panoramic camera recognition positioning, projection positioning |
| Tool Head Options | Oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V cutting knife, drag knife, creasing wheel, dotted line knife, punching, brush |
| Multifunctional Head | Swiss imported knife with vibration full cutting, vibration half cutting and cursor location |
| Key Features | Multi-zone vacuum adsorption, CCD contour recognition options, configurable tool head setup |
Application Suitability
| Application | Material or Output |
|---|---|
| Automotive interior trim and seating | Multi-layer leather, synthetic fabric and foam composites |
| Footwear and luggage production | Natural leather, PU, EVA, shoe material, non-woven fabric |
| Garment and textile cutting | Woven fabric, clothing cloth, carpet, sponge, XPE |
| Gasket and sealing pad fabrication | Rubber, PTFE, ETFE, fiberglass, composite gasket sheets |
| Packaging and carton sample making | Corrugated cardboard, plastic box, PVC, PP, PE |
| Soft home furnishings | Foam board, sponge, PU, textile, curtain and upholstery fabric |
| Graphic advertising and printing | Sticker, film, vinyl, corrugated board for display stands |
When a 20–80 mm Thickness Claim Misses the Real Story
Cutting depth only matters against the specific material stack you are feeding the table.
A buyer once specified an oscillating knife machine purely on working area and quoted cutting range, only to discover the blade could not penetrate a leather-foam composite at production speed. The manufacturer had tested on single-layer EVA. Material density, composite layering and adhesive bonding all change the effective cutting load. As a CNC Oscillating Knife Cutting Machine manufacturer, we run sample cuts on the buyer’s own material before the order is confirmed, documenting edge quality, penetration and achievable speed in a written report. [NEED_CITE: composite material density and its effect on oscillating knife cutting depth]
Frame Rigidity That Holds Tolerance Over Years
The RT-D2516/RT-S2516 frame is built from thick-walled seamless steel that undergoes high-temperature tempering before final machining. This process relieves internal stresses introduced during welding, so the frame does not warp after months of vibration cycles. The entire structure is finished on a CNC machining center, which guarantees the flatness and squareness that the linear guides and ball screws depend on. When the frame holds geometry, the ≤0.1 mm repeated accuracy is not just a spec-sheet number — it is what you see on the cutting table day after day.
Vacuum Table Engineering for Uneven and Small Parts
The magnesium-aluminum alloy table surface goes through fluorocarbon PVDF powder spraying, anodic oxidation and hard oxidation. These processes create a surface that resists wear from abrasive materials like fiberglass and carpet while maintaining the flatness vacuum adsorption requires. The 7.5 kW vacuum pump provides the suction force, but what matters more is how the table zones are configured. Small parts such as gaskets or shoe components tend to lift at the edges during high-speed cutting if the vacuum zone is larger than the part footprint. We configure zone layout based on the buyer’s typical part sizes before the machine ships.
Reading the Specs That Actually Affect Your Production
The 800–1200 mm/s translational velocity defines how fast the tool head moves between cuts, but actual throughput depends on material, nesting density and cut path complexity. The Swiss imported oscillating knife delivers full cutting and half cutting (kiss-cut) on a single head, so a packaging sample maker can score and cut corrugated board without a tool change. Delta digital servo motors paired with iwin linear guides provide the motion control needed to hold ≤0.1 mm accuracy across the full 1600×2500 mm envelope. The HP-GL compatible instruction system means the machine accepts file formats common in existing CAD and nesting workflows. CCD camera options — from mark point positioning to panoramic recognition — handle printed contour work where registration marks must be tracked at production speed. [NEED_CITE: HP-GL format compatibility in industrial cutting software workflows]
The Cost of Choosing the Wrong Tool Head
I once configured a vibrating knife setup for a customer making automotive seat covers based on the leather samples they sent. The cuts were clean and the edges sharp. Then production started on the actual composite material — leather bonded to a foam layer — and the standard oscillating knife compressed the foam instead of shearing through it. The entire first batch had to be re-cut. The fix was switching to a high-power vibrating knife with adjusted stroke and pressure. Wrong tool head selection leads to ragged edges on textiles, crushed foam cores, incomplete cuts on dense gasket material, and rejected parts that nobody notices until the downstream assembly line stops. [NEED_CITE: material-specific tool head selection for oscillating knife cutting systems]
Why Source This Machine from the Build Floor Up
We design and manufacture both the knife cutting system and the laser cutting equipment in-house, so a buyer can match the cutting method to the material rather than being forced into one technology. The frame, motion components, vacuum table and tool heads are all configured under one roof for the RT-D2516/RT-S2516. Each machine is specified against the buyer’s stated material type, thickness and daily volume, not sold from a fixed catalog page. Software file format compatibility is verified before the order enters production. Sample cutting on the buyer’s own material is standard procedure, not an optional extra. We confirm voltage, plug type and control language for the destination market before shipment, avoiding the rewiring and reprogramming that delays commissioning. [NEED_CITE: electrical standards and plug configurations for industrial machinery exports]
Documentation & Verification
- Machine specification sheet with complete tool head and table configuration list
- Electrical schematic confirming voltage and frequency for destination market
- Sample cutting report on buyer’s own material showing edge quality and speed
- Factory test record documenting accuracy, vacuum performance and safety device checks
- Software licence and file format compatibility note matching buyer’s CAD workflow
- Operation and maintenance manual with spare parts list in buyer’s control language
Installation, Commissioning & Support
- Floor space planning based on the 3450×2300×1250 mm machine footprint and material infeed clearance
- Dedicated electrical circuit provision matching the 9 kW rated power and 380V±10% supply requirement
- Vacuum pump commissioning and multi-zone suction calibration for the buyer’s typical part geometry
- Tool head setup and cutting parameter tuning on buyer’s production material during on-site commissioning
- Operator training covering HP-GL file import, nesting workflow and CCD camera mark point registration
- Scheduled maintenance plan for linear guides, synchronous belts and oscillating knife blade replacement
Preparing Your Inquiry
To match the right configuration, share your material type, maximum thickness, composite layer structure and typical sheet dimensions. Include your daily cutting volume and the file formats your design team currently uses. Confirm the local voltage and frequency at your facility, and whether control panel language requirements differ from English or Chinese.
Frequently Asked Questions
Q: How is cutting thickness verified against my specific material before I commit to the order?
A: We require buyers to send actual production material — not catalog samples — so we can run cutting tests across the full material stack. The result is a written sample cutting report documenting edge quality, complete penetration, achievable speed and recommended tool head. This report is shared before the quotation is finalized.
Q: What voltage, plug and control language options are confirmed before shipment?
A: We confirm the destination market’s voltage, frequency and plug standard before the machine enters production. The 380V±10% system can be configured to match local supply. Control panel language and software interface language are set according to buyer requirements and documented in the specification sheet before shipping.
Q: How is the vacuum table zoned to prevent small parts from lifting during cutting?
A: The magnesium-aluminum alloy vacuum table is configured with zone sizes matched to the buyer’s typical part dimensions. When cutting small gaskets or shoe components, oversized zones allow air leakage that reduces holding force. We design the zoning layout based on your production part range and verify suction performance during the factory test.
Q: What tool head is recommended for my material and how is edge quality validated?
A: Tool head selection depends on material type, thickness and whether the job requires full cut, kiss-cut or creasing. Options include oscillating knife, pneumatic knife, drag knife, creasing wheel and punching tools. Edge quality is validated during sample cutting on the buyer’s own material, and the recommended configuration is documented before the order proceeds.
Q: Can I visit the factory to inspect the frame build process and motion assembly?
A: Factory visits are available during production. Buyers can inspect the thick-walled seamless steel frame after high-temperature tempering, observe CNC machining center finishing, and witness motion assembly with Delta servo motors and iwin linear guides. A factory test on the buyer’s material can be scheduled during the visit to verify performance before shipment.
You may also like







商品评价
Clear filtersThere are no reviews yet.