





-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

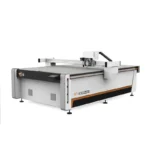
Purpose-Built Frame Engineering — The CLD2516 welded steel structure undergoes high-temperature stress relief, ensuring dimensional stability across the full 1600×2500mm working envelope during continuous cutting shifts.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | CNC Oscillating Knife Cutting Table |
| Working Area | 1600mm × 2500mm |
| Machine Dimensions | 3450 × 2300 × 1250mm |
| Rated Power | 6.6kW |
| Voltage | 380V ±10% |
| Vacuum Pump | 7.5kW |
| Translational Velocity | 800–1200 mm/s |
| Cutting Thickness Range | 20–80mm (varies by material type and density — confirm with sample test) |
| Repeatability | ≤0.1mm |
| Servo Motor | Taiwan Delta digital servo |
| Linear Guide | Taiwan Hiwin imported linear guide |
| Working Table | Aluminum alloy honeycomb flat vacuum adsorption platform with partition zoning |
| Tool Head | Swiss imported oscillating knife — full-cut, half-cut and cursor positioning |
| Transmission System | Digital servo motor, imported linear guide, synchronous belt, ball screw |
| Conveyor Belt | Germany imported |
| Auto Feeding | Yes |
| Safety Device | Infrared sensors and emergency stop |
| Supported File Formats | PLT, DXF |
| Instruction System | HP-GL compatible format |
| Software Language Options | English, Russian, Italian, Chinese (custom languages available) |
| Machine Frame | Welded thick square seamless steel with high-temperature treatment |
| Material Fixing | Vacuum partition adsorption |
| Warranty | 1 year (parts free, buyer covers shipping; engineer dispatch free, buyer covers travel and accommodation) |
Application Suitability
| Application | Material or Output |
|---|---|
| Carton and packaging sample making | Corrugated board, card stock, greyboard for short-run prototypes and die-free small-batch cartons |
| Sticker and label contour cutting | Vinyl, self-adhesive film, printed label sheets requiring precise contour following |
| Signage and billboard production | Foam board, PVC sheet, lightweight display board for point-of-sale and exhibition graphics |
| Leather goods fabrication | Genuine leather, synthetic PU/PVC leather, composite leather for bags, footwear uppers and accessories |
| Flexible composite processing | Sponge composite leather, fabric, silicone rubber, soft glass requiring clean edge without burn marks |
Why Specified Working Area Is Not Enough for a CNC Knife Cutting Machine Manufacturer to Guarantee Results
Material density and vacuum zoning determine whether a machine actually cuts at the stated thickness, not just the frame dimensions.
A buyer who selects a cutting table based purely on working area often discovers that the vacuum hold-down cannot secure small or lightweight parts during oscillating knife travel. The result is lifted edges, ragged cuts, and rework that slows the entire production cell. I have seen this happen when a gasket producer assumed a standard 7.5kW vacuum pump would handle thin PTFE sheets across the full table, only to find that un-zoned suction left corner pieces shifting mid-cut [NEED_CITE: vacuum hold-down requirements for thin flexible materials]. The real question is whether the vacuum partition layout matches the size and weight distribution of the parts you actually produce.
Frame Rigidity and Its Role in Repeatable Cut Accuracy
The CLD2516 frame uses thick square seamless steel welded into a single structure, then subjected to high-temperature stress relief treatment. This process reduces residual welding stress that would otherwise cause gradual frame distortion over months of vibration-heavy oscillating cutting. For a CNC knife cutting machine manufacturer building equipment for continuous production environments, frame stability directly governs whether the ≤0.1mm repeatability specification holds after thousands of cutting hours.
How Vacuum Partition Zoning Prevents Small-Part Lift
The aluminum alloy honeycomb table surface is divided into independently controlled vacuum zones. When cutting small gaskets or narrow label strips, only the active zone beneath the material needs suction, concentrating hold-down force where the knife is working. This prevents the common problem of distributed suction being too weak across the full table area, which causes thin or lightweight pieces to lift ahead of the blade and produce incomplete cuts [NEED_CITE: vacuum zoning effectiveness for small part nesting].
Matching the Swiss Oscillating Knife to Material Behavior
The Swiss imported oscillating knife head delivers full-cut, half-cut, and cursor positioning functions in a single tool setup. Oscillating motion at high frequency allows the blade to slice through compressible materials like sponge composite leather or foam without crushing the cross-section — a drag knife would compress and tear these same materials. Cutting thickness ranges from 20mm to 80mm depending on material density, and the actual achievable depth must be confirmed by test cut on the specific stock you plan to run.
The Cost of Skipping Material-Specific Configuration
Choosing a flatbed cutting table without specifying the tool head angle, blade type, and vacuum zone layout for your actual material leads to compounding problems. Ragged edges on leather uppers require secondary trimming that adds labor to every piece. Crushed foam gaskets fail sealing tests at the assembly stage. Vinyl stickers that shift during contour cutting produce misaligned kiss-cuts, wasting printed sheets. These downstream costs accumulate quietly because they show up as scrap and rework rather than a single machine failure event [NEED_CITE: hidden production costs from incorrect cutting tool configuration].
What the Factory Design Team Brings to Each Order
The CLD2516 is produced in a facility that engineers both knife and laser cutting systems under one roof, meaning the oscillating knife configuration is specified deliberately rather than defaulting to a single platform. Each tool head and vacuum table layout is matched to the buyer’s material type and production volume before the order is finalized. The Taiwan Delta servo and Hiwin linear guide combination is selected for the specific travel dynamics of knife cutting — high acceleration with controlled deceleration at direction changes. Software file format compatibility with existing PLT and DXF workflows is confirmed before shipment, so the machine integrates into the buyer’s current nesting and production pipeline. Sample cutting on the buyer’s own material is conducted and documented before commitment, verifying edge quality, achievable thickness, and cutting speed on the actual stock.
Documentation & Verification
- Machine specification sheet confirming working area, power rating and voltage configuration for your facility
- Electrical schematic with voltage confirmation matching your 380V ±10% supply requirements
- Tool head and table configuration list specifying knife type, blade angle and vacuum zone layout for your material
- Sample cutting report on your own material showing edge finish, cutting depth and achieved speed
- Factory test record documenting repeatability measurement and vacuum partition performance before dispatch
- Software license and file format compatibility note confirming PLT/DXF import with your nesting workflow
Installation, Commissioning & Support
- Requires level concrete floor with minimum clearance around the 3450 × 2300mm machine footprint for material loading access
- Dedicated 380V ±10% circuit rated for the combined 6.6kW machine and 7.5kW vacuum pump draw
- Delivered with conveyor and auto-feeding system pre-assembled; table leveling and vacuum zone calibration on site
- First-run parameter tuning for your specific material thickness, blade oscillation frequency and vacuum zone pressure
- Operator training covering tool head changeover, file import workflow and vacuum partition zone selection
- Spare blade and wear part list provided with recommended reorder intervals based on your material abrasiveness
What We Need to Specify Your Configuration
To recommend the correct tool head, vacuum layout and software setup, please share your material type, typical sheet dimensions, and the thickness range you plan to cut. Include your facility voltage and frequency, preferred control language, and the file formats your design team currently uses for nesting. If you are replacing an existing cutting cell, let us know the upstream printing or downstream assembly equipment so we can match throughput expectations.
Frequently Asked Questions
Q: How is the oscillating knife tool head selected for my specific material?
A: The blade angle, oscillation frequency and knife type are chosen based on material density, thickness and the edge quality your product requires. Compressible materials like foam need high-frequency oscillation to avoid crushing, while dense rubber gaskets require a stiffer blade. We confirm the selection through sample cutting on your actual material before the order proceeds.
Q: What electrical and language details are confirmed before the machine ships?
A: Your facility voltage, frequency and plug type are verified against the 380V ±10% baseline, and an electrical schematic is issued for your electrician to review. The control software language — English, Russian, Italian, Chinese or a custom option — is set and confirmed so the operator interface is ready on day one.
Q: Can I send my own material for sample cutting before placing the order?
A: Yes. Send us representative sheets of your production material, and we run test cuts on the CLD2516 at our factory. You receive a sample cutting report documenting edge finish, achievable cutting thickness and speed on your specific stock, so you can evaluate results before committing to the purchase.
Q: How does vacuum partition zoning handle small parts that tend to lift?
A: The honeycomb vacuum table is divided into independently controlled zones. When cutting small or lightweight pieces, suction is concentrated in the active zone beneath the cutting path rather than spread across the entire table. This focused hold-down prevents thin vinyl strips, labels and narrow gaskets from lifting ahead of the oscillating knife.
Q: What custom configuration options can the factory design team provide?
A: The engineering team can adjust conveyor belt length, auto-feeding roller configuration, vacuum zone layout and software language to match your production workflow. Special tool head combinations — pairing the oscillating knife with a creasing wheel or pen marker — are configured based on the secondary operations your product requires after cutting.
You may also like







商品评价
Clear filtersThere are no reviews yet.