



-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

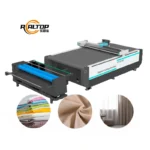
Factory-built frame and motion integration — the RT-D2516/RT-S2516 chassis is overall-welded and machined on imported milling equipment before assembly, keeping guide rail flatness within tolerance from day one.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Vacuum Pump | 7.5 kW |
| Cutting Thickness | ≤50 mm (varies with material density and layer count) |
| Translational Velocity | 800–1200 mm/s |
| Repeated Accuracy | ≤0.1 mm |
| Table Type | Flat working table with high-density felt surface |
| Tool Head | Swiss imported knife with vibration full cutting, half cutting and cursor location |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor | Panasonic (Delta option available) |
| Guide Rail | Taiwan Hiwin rail |
| Conveyor Belt | Germany imported |
| Frame | Overall welding process, imported milling machine processing |
| Safety Device | Infrared sensors |
| Instruction System | HP-GL compatible format |
| Voltage | 380V ±10% |
| Software Language Options | English, Russian, Italian, Chinese (special languages customizable) |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Garment and footwear production | Multi-layer fabric, leather, synthetic textiles |
| Automotive interior trimming | Composite leather, sponge-backed materials, foam |
| Bag and luggage manufacturing | PVC, soft glass, silicon sheets |
| Gasket and seal fabrication | Rubber, silicone, flexible composites |
| Packaging sample making | Corrugated board, carton stock |
| Home furnishing upholstery | Foam composites, coated textiles |
Why Material Thickness Changes the Machine You Actually Need
Cutting depth is not a single number — it depends on material density, layer count and tool head frequency.
A common mistake in this equipment class is selecting a CNC oscillating knife cutting machine manufacturer based on working area alone, then discovering the vibration frequency cannot handle the actual stock thickness on the shop floor. I once visited an automotive interior supplier where single-layer canvas cut cleanly during the sample test, but multi-layer coated nylon caused edge fraying and vacuum lift at production speed. The entire batch had to be reworked. [NEED_CITE: material density effects on oscillating knife cutting performance]
When a distributor or importer evaluates a source factory, the conversation must start with the buyer’s real material stack — not a generic thickness claim.
Frame Construction and Motion Accuracy
The RT-D2516/RT-S2516 frame goes through overall welding followed by machining on an imported milling system, which establishes the reference surface for the Hiwin guide rails. This matters because rail flatness directly controls positional accuracy across the 1600 × 2500 mm working envelope. A CNC oscillating knife cutting machine manufacturer that skips post-weld stress relief risks rail misalignment after months of vibration loading.
Vacuum Table Design and Small-Part Retention
The flat working table uses a high-density felt surface over an aluminum base with internal wind-channel routing. The 7.5 kW vacuum pump pulls through this structure to hold material flat during cutting. For small gasket or pattern pieces, even suction distribution prevents lift at the blade exit point — a frequent cause of ragged edges on thin rubber and foam. Zone control on the table allows operators to activate only the sections under the current cut path, concentrating suction where it matters. [NEED_CITE: vacuum table zoning requirements for small part cutting]
Reading the Specs That Matter on the Floor
The ≤0.1 mm repeated accuracy figure comes from the combination of Panasonic digital servo motors and ball-screw drive on the critical axes. In practice this means nested pattern pieces stay within tolerance across a full shift of continuous cutting. The 800–1200 mm/s translational velocity range gives operators room to slow down on tight contours while maintaining throughput on long straight runs. The Swiss imported oscillating knife handles both full-cut and half-cut operations, which is essential when scoring fold lines on packaging samples without penetrating the backing. HP-GL format compatibility lets the control system accept files from most mainstream nesting software without intermediate conversion.
What Happens When the Tool Head Is Wrong for the Stock
Choosing an incorrect tool head for the material produces visible defects — crushed foam cores, frayed textile edges, or incomplete cuts through layered composites. On an oscillating knife system, blade frequency must match material resilience; a frequency that works on single-ply leather will tear through multi-layer coated nylon. Buyers who skip the material-specific tool head conversation at inquiry stage often discover the mismatch only after installation, when re-tooling means downtime and replacement blade costs. [NEED_CITE: oscillating knife frequency matching to composite material density]
Why Source Directly from the Build Floor
The RT-D2516/RT-S2516 is designed and assembled under one roof, which means the engineering team that specifies the frame weld pattern also signs off on the motion assembly. An in-house design and production setup covering both the mechanical structure and the tool head integration allows configuration changes — table size, vacuum zoning, servo brand — without waiting on third-party suppliers. Sample cutting on the buyer’s own material runs on the same production floor where the machine is built, so the test reflects the actual configuration that ships. Voltage, plug type and control language are confirmed before the electrical panel is closed, not after the crate is packed. For distributors evaluating OEM capability, the factory can adjust branding, documentation language and software interface to match the destination market.
Documentation & Verification
- Machine specification sheet listing tool head and table configuration matched to your material type
- Electrical schematic with voltage and frequency confirmed for your local supply standard
- Factory test record documenting cut quality on your supplied material sample
- Sample cutting report showing edge condition and dimensional accuracy on your stock
- CE declaration and software licence note with file format compatibility details
- Spare parts list with part numbers for blades, felt and vacuum consumables
Installation, Commissioning & Support
- The 3450 × 2300 × 1250 mm footprint requires a level concrete pad with clearance on three sides for material loading
- 380V ±10% supply needs a dedicated circuit breaker sized for the combined 9 kW machine and 7.5 kW vacuum pump draw
- Control box mounts on the fuselage with high-flexibility cables, reducing external wiring during commissioning
- First-run parameter setup includes vacuum zone mapping, blade depth calibration and servo tuning for the selected material
- Operator training covers tool head changeover between round knife, marking pen and feeder attachments
- High-density felt table surface is a wear item — replacement schedule depends on daily cutting hours and abrasive material content
Before You Request a Quote
Send the material type, actual thickness range and typical sheet dimensions you will run. Specify the daily cutting volume and whether your workflow uses nesting software that outputs HP-GL. Confirm the local voltage and frequency standard, the preferred control language, and whether you need the machine configured for single-head or multi-tool operation. If you have printed contour work, note whether registration marks are used so the configuration can account for recognition requirements.
Frequently Asked Questions
Q: How does the factory verify cutting capacity for a specific material and thickness before order?
A: The buyer ships a sample of the actual production material to the factory. The RT-D2516/RT-S2516 is set up with the proposed tool head and vacuum configuration, then test cuts run at production speed. The resulting sample cutting report documents edge quality, dimensional accuracy and any adjustments made, so the buyer sees real performance before committing to the order.
Q: What OEM customization is available for voltage, language, table size and tool configuration?
A: Voltage is configurable to match destination market standards. Control software language options include English, Russian, Italian and Chinese, with special languages available on request. The working area and tool head selection are specified per material application. These choices are locked in before the electrical panel and software are finalized, not adjusted after shipment.
Q: How are motion components and frame quality controlled during production?
A: The frame undergoes overall welding and then passes through an imported milling machine that machines the guide rail and rack mounting surfaces to flatness tolerance. Hiwin guide rails and ball screws are installed and measured for positional accuracy. The Panasonic or Delta servo system is tuned with the assembled drive train before the machine leaves the production floor.
Q: What documentation ships with the machine for import clearance and local compliance?
A: Each RT-D2516/RT-S2516 ships with a CE declaration, machine specification sheet, electrical schematic matching the confirmed voltage, operation and maintenance manual, software licence with file format compatibility note, and a factory test record. These documents cover the standard requirements for customs clearance and local machinery compliance in most export markets.
Q: What is the spare parts supply policy and lead time for distributors?
A: A spare parts list with part numbers is included at shipment, covering consumables like oscillating blades, felt table covers and vacuum components. The factory maintains stock of standard wear items and processes distributor orders on a typical multi-week lead basis. Custom configuration parts are quoted with lead time at the time of the original machine order.
You may also like







商品评价
Clear filtersThere are no reviews yet.