







-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

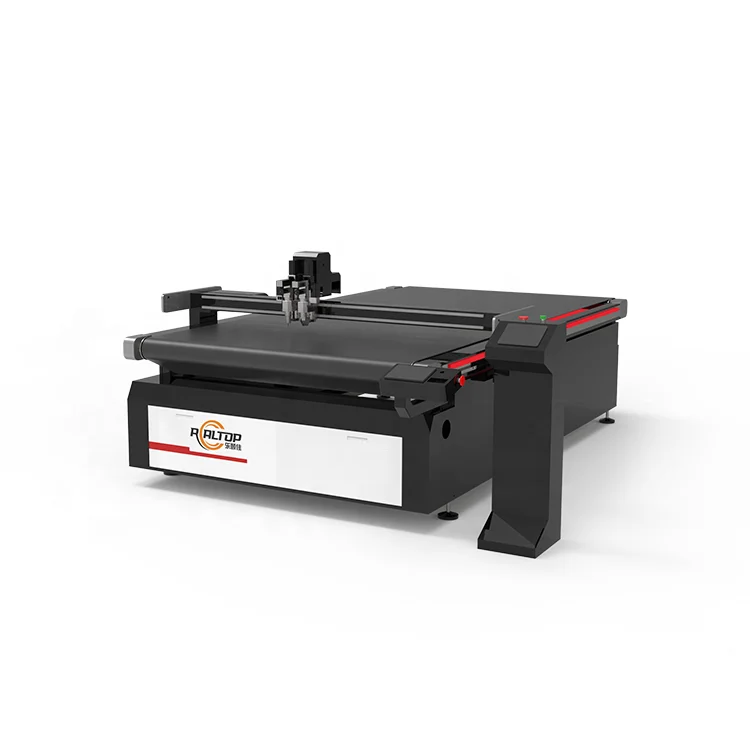
Core factory build — In-house design and production of the RT-D2516/RT-S2516 frame, motion system and tool head integration, so distributors and importers source from the manufacturer rather than a trading intermediary.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600 × 2500 mm |
| Machine Size | 3450 × 2300 × 1250 mm |
| Rated Power | 9 kW |
| Working Table | Flatted working table with auto feeding and vacuum table |
| Multifunctional Head | Swiss imported knife with vibration full cutting, vibration half cutting and cursor location function |
| Translational Velocity | 800 – 1200 mm/s |
| Cutting Speed | 200 – 800 mm/s (according to different cutting materials) |
| Repeated Accuracy | ≤ 0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw (imported) |
| Servo Motor | Japanese Yaskawa |
| Guide Rail | Taiwan Hiwin |
| Conveyor Belt | Germany imported |
| Instruction System | HP-GL compatible format |
| Voltage | 380V ± 10% |
| Vacuum Pump | 7.5 kW |
| Safety Device | Infrared sensors |
| Standards | CE declaration |
Application Suitability
| Application | Material or Output |
|---|---|
| Garment and footwear production | Multi-layer fabric, composite leather, flexible clothing materials |
| Leather goods manufacturing | Natural and synthetic leather, sponge composite leather |
| Automotive interior components | PVC, soft glass, silicone, rubber for dash and door panel gaskets |
| Industrial gasket fabrication | Rubber, silicone, composite foam sheets |
| Textile and non-woven processing | Non-woven mesh, technical textiles, layered cloth |
Why "Cutting Speed 200–800 mm/s" Needs a Material Qualifier
The speed range only holds meaning when tied to the exact material density and thickness being processed.
Buyers comparing CNC oscillating knife cutting machine manufacturer quotes often focus on the headline speed number, then discover on the shop floor that a coated composite runs at a fraction of the speed used for plain cotton. The 200–800 mm/s window on the RT-D2516/RT-S2516 is material-dependent, and the correct operating point is determined during factory sample cutting on the buyer’s own stock. Skipping that step leads to ragged edges on dense layers or crushed foam cores on lighter passes. [NEED_CITE: material-dependent cutting speed benchmarks for oscillating knife systems]
Frame Construction and Motion Component Sourcing
The RT-D2516/RT-S2516 frame is built and assembled in-house, giving the factory direct control over weld stress-relief and gantry alignment. Japanese Yaskawa digital servo motors drive the axes through Taiwan Hiwin linear guides, delivering ≤ 0.1 mm repeatability across the full 1600 × 2500 mm working area. Because the CNC oscillating knife cutting machine manufacturer handles both frame and motion integration under one roof, tolerance stacking between sub-assemblies is eliminated before the machine leaves the factory floor.
Vacuum Table Zoning and Small-Part Holding
A 7.5 kW vacuum pump feeds a configurable vacuum table, allowing zones to be isolated so small garment pattern pieces or automotive gaskets stay flat during the cut. Without zoning, a large open table loses suction on small nested parts, causing material lift and edge deviation. The RT-D2516/RT-S2516 table layout is specified at order stage to match the buyer’s typical nest geometry, preventing rework after installation. [NEED_CITE: vacuum table zoning effects on small-part cutting accuracy]
Specifying Tool Head and Drive for Material Response
The Swiss imported oscillating knife head offers both full-cut and half-cut vibration modes. Full-cut handles dense composites and multi-layer leather stacks, while half-cut scores PVC or soft glass for folding without severing the sheet. Paired with the Yaskawa servos and imported ball screws, the head maintains consistent stroke frequency across long cutting paths. The HP-GL compatible instruction system accepts nesting files from common CAD platforms, reducing file-format friction between the buyer’s design office and the machine controller.
The Cost of a Mismatched Tool and Material Pairing
Choosing a standard drag knife for sponge composite leather produces frayed edges that require manual trimming downstream. On the RT-D2516/RT-S2516, specifying the wrong vibration mode for a coated textile causes the blade to skate across the coating rather than penetrate, generating scrap and delaying delivery schedules. The factory sample cutting step catches these mismatches before the machine is built, avoiding two weeks of lost production time on the buyer’s line. [NEED_CITE: tool head selection errors and downstream rework costs in textile cutting]
Sourcing from the Manufacturer Rather Than an Intermediary
In-house design means the RT-D2516/RT-S2516 frame, motion and tool head are engineered as a single system, not assembled from catalog parts by a third party. The factory configures voltage, plug type and control language before shipment, eliminating the voltage mismatch problem that surfaces only after the container arrives. OEM customization covers working area adjustments, conveyor integration and branding on panels for distributor markets. Sample cutting on the buyer’s actual material is performed and documented before the order is locked, providing physical proof of edge quality rather than relying on brochure claims.
Documentation & Verification
- Machine specification sheet listing RT-D2516/RT-S2516 tool head and table configuration per order
- Electrical schematic with 380V ± 10% wiring diagram and Yaskawa servo connection detail
- Factory test record showing ≤ 0.1 mm repeatability measurement on buyer’s material sample
- Software licence and HP-GL file format compatibility note confirmed before dispatch
- Spare parts list covering Swiss knife blades, conveyor belt segments and vacuum pump consumables
- Packing photographs documenting crating condition prior to container loading
Installation, Commissioning & Support
- 3450 × 2300 mm footprint requires level concrete floor with anchor points for machine stabilizers
- 9 kW rated power needs dedicated 380V three-phase circuit with isolator within reach of the control cabinet
- Gantry and conveyor belt arrive pre-assembled; vacuum table zones are connected and tested on-site
- First-run calibration sets Yaskawa servo parameters and Hiwin rail pre-load for the 1600 × 2500 mm travel range
- Operator training covers HP-GL file import, vacuum zone selection and Swiss knife blade change procedure
- Maintenance schedule covers guide rail lubrication, ball screw inspection and vacuum pump filter replacement
Preparing Your Material Brief for Quotation
Send fabric type, coating details and the thickest composite you plan to run so the correct oscillating knife mode is specified. State your local voltage and frequency along with preferred control panel language to avoid post-shipment rewiring. If you require OEM branding or custom conveyor length for your distribution market, include those requirements in the initial inquiry.
Frequently Asked Questions
Q: What build quality and frame construction does the core factory deliver?
A: The RT-D2516/RT-S2516 frame is welded, stress-relieved and machined in-house. Gantry alignment is verified before motion components are mounted, and the entire assembly runs through a factory acceptance test that checks ≤ 0.1 mm repeatability across the full 1600 × 2500 mm working area before crating.
Q: Which motion components are sourced and how are they specified?
A: Japanese Yaskawa digital servo motors drive the axes through Taiwan Hiwin linear guides and imported ball screws. The combination is chosen to maintain cutting accuracy on flexible materials where belt stretch would otherwise cause pattern drift on multi-layer textile stacks.
Q: How is voltage, plug type and control language confirmed before shipment?
A: The factory records the buyer’s 380V ± 10% requirement, plug standard and preferred HMI language on the specification sheet before production begins. The electrical schematic is shared for approval, preventing rewiring costs or controller confusion after the machine arrives at its destination.
Q: What OEM capability and customization range does the factory offer?
A: Beyond standard RT-D2516/RT-S2516 configuration, the factory can adjust working area dimensions, add conveyor extensions and apply distributor branding to machine panels. Tool head selection and vacuum table zoning are matched to the buyer’s target material profile for their specific market segment.
Q: What documentation accompanies the machine at shipment?
A: Each unit ships with a specification sheet, electrical schematic, factory test record, CE declaration, operation and maintenance manual, software licence note, spare parts list and packing photographs. These documents support import compliance and enable the buyer’s service team to begin maintenance from day one.
You may also like







商品评价
Clear filtersThere are no reviews yet.