





-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

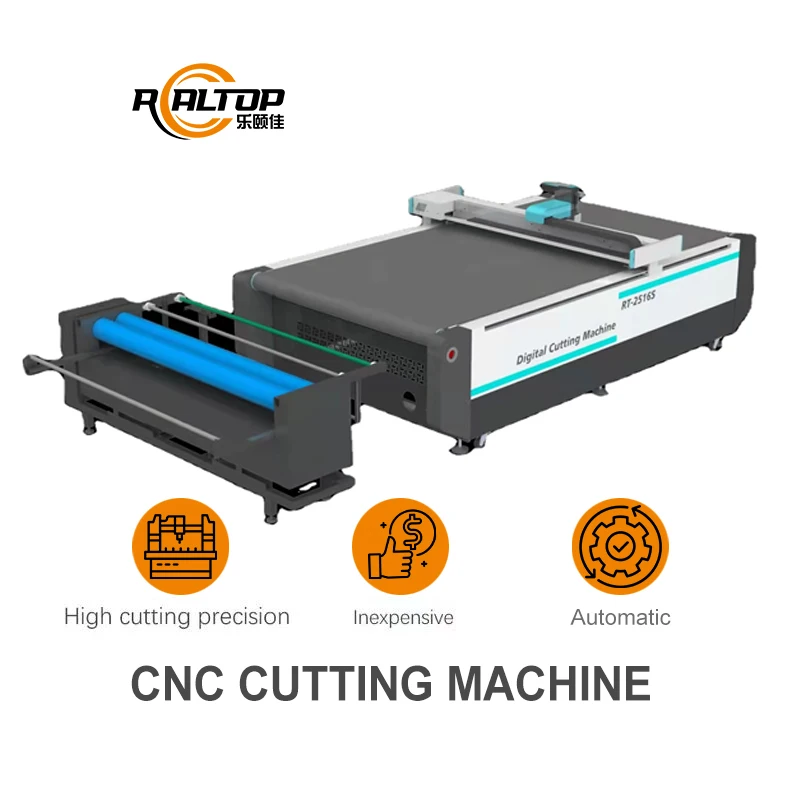
In-house knife system engineering — REALTOP matches tool head and table configuration to the buyer’s exact material, avoiding the common trap of forcing one cutting method across incompatible substrates.
Technical Specifications
| Parameter | Value |
|---|---|
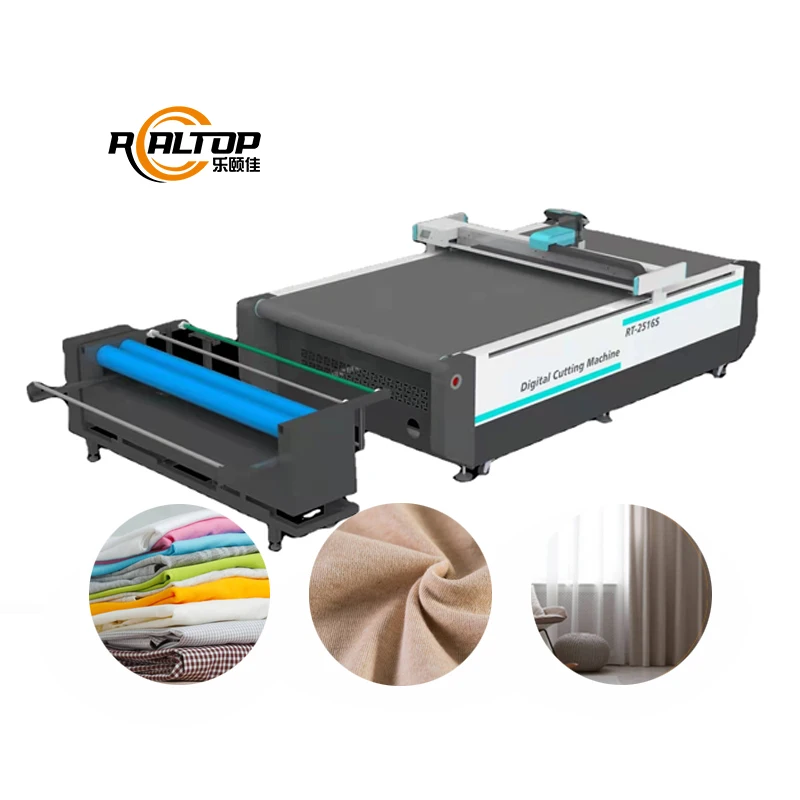
| Model | RT-D2516/RT-S2516 |
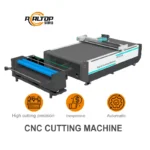
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600×2500 mm |
| Overall Dimensions | 3450×2300×1250 mm |
| Rated Power | 9 kW |
| Voltage | 380V ±10% |
| Control System | CNC (HP-GL compatible format) |
| Tool Head Options | Oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V-cutting knife, drag knife, creasing wheel, dotted line knife, punching, brush |
| Visual Positioning | Small CCD camera mark point positioning, panoramic camera recognition, projection positioning |
| Cutting Thickness Range | 20 mm – 80 mm (basis not stated in source — confirm material type and density) |
| Max Cutting Thickness | ≤100 mm (varies with material) |
| Translational Velocity | 800–1200 mm/s |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw (imported) |
| Servo Motor Brand | Delta (Panasonic optional) |
| Linear Guide | Taiwan Hiwin rail |
| Working Table | Magnesium-aluminum alloy vacuum adsorption table, fluorocarbon PVDF powder spraying, anodic oxidation, hard oxidation |
| Vacuum Pump | 7.5 kW, integrated aviation aluminum shell, built-in silencer sponge |
| Conveyor Belt | Germany imported |
| Safety Devices | Infrared induction blocking, anti-collision, emergency stop |
| Language Options | English, Russian, Italian, Chinese (special languages customizable) |
| Assembly State | Fully assembled |
| Warranty | 1 year (lifetime technical support) |
| Operating Features | Full size cutting, kiss cutting, slot milling, punching, inkjet, drawing marking |
| Certification | CE (declaration where applicable) |
Application Suitability
| Application | Material or Output |
|---|---|
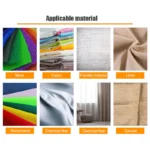
| Garment and footwear production | Multi-layer fabric, shoe material, luggage material, non-woven fabric, clothing cloth |
| Automotive interior and gasket manufacturing | Composite materials, sponge, PU, EVA, XPE, rubber, sealing pads |
| Packaging and carton sample making | Corrugated cardboard, cardboard, plastic box, film, sticker |
| Soft furnishings and carpet processing | Carpet, foam board, PVC, textile, soft home furnishing fabrics |
| Graphic advertising and printing | Vinyl, board, sticker, printed film for contour cutting |
| Sports and outdoor product fabrication | Fiberglass, PTFE, ETFE, PE, PP, composite performance materials |
What Buyers Discover After the Machine Arrives
Most purchasers specify a CNC oscillating knife cutting machine manufacturer based on working area alone, assuming any flatbed can handle any material within that footprint. Cutting depth capacity is not a function of table size — it depends on knife stroke, vacuum zoning and blade geometry matched to material density.
I have watched buyers pay for a 1600×2500 mm bed only to find their six-layer composite automotive material lifts during cutting because the vacuum zones were configured for single-ply fabric. The problem is never visible in the catalog photo. It surfaces on the first production day when small parts shift and the blade catches, leaving ragged edges across a full sheet of expensive material. [NEED_CITE: vacuum hold-down requirements for multi-layer composite cutting]
The cost of this mismatch is measured in re-cuts, scrapped material and days of on-site troubleshooting that could have been resolved with a proper sample test before the machine left the factory floor.
Tool Head Selection Defines Edge Quality, Not Just Speed
The multifunctional head on the RT-D2516/RT-S2516 accepts the full tooling range — oscillating knife, drag knife, creasing wheel, punching and marking tools. The critical decision is which combination matches the buyer’s actual material stack. A Swiss imported oscillating knife handles high-frequency vibration cutting for dense foam and composite layers, while a drag knife suits thinner vinyl and sticker contouring. A CNC oscillating knife cutting machine manufacturer that ships a single default tool head forces the operator to compromise on edge finish across different jobs.
Vacuum Zoning and Table Flatness Determine Small-Part Yield
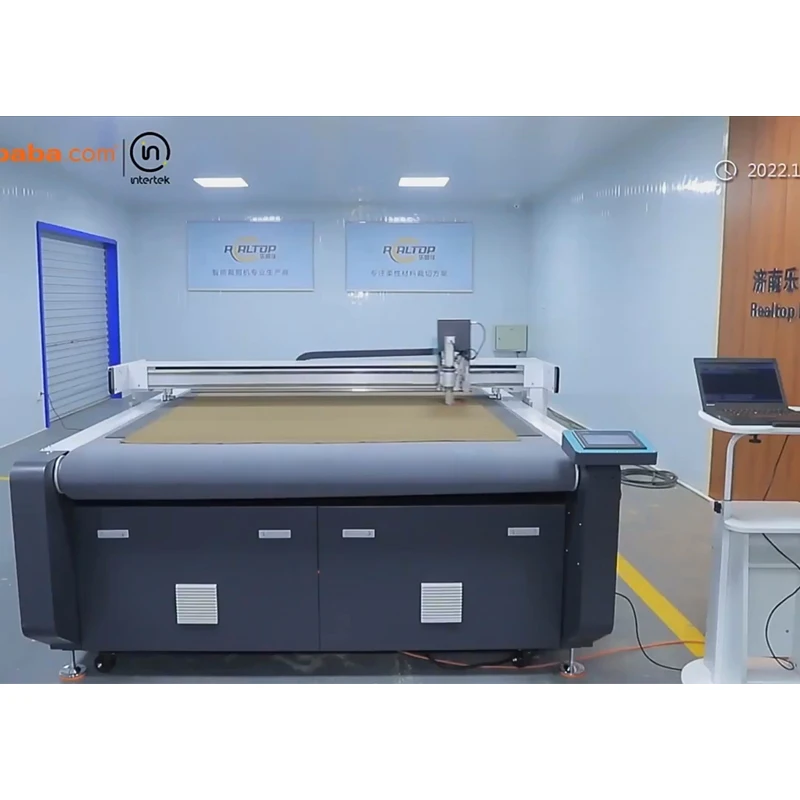
The magnesium-aluminum alloy table surface receives PVDF powder spraying and hard oxidation treatment, which maintains flatness under repeated vacuum cycles. The 7.5 kW vacuum pump with aviation aluminum housing delivers suction across the full 1600×2500 mm bed. But flatbed cutting of nested small parts — gaskets, shoe components, garment panels — demands that vacuum zones isolate areas where material has already been cut away. Without proper zoning, airflow escapes through cut lines and adjacent parts lose hold-down force mid-cycle. [NEED_CITE: vacuum table zoning standards for CNC flatbed digital cutting systems]
Reading the Specs That Actually Matter on the Floor
The ≤0.1 mm repeated accuracy figure comes from Delta digital servo motors paired with Taiwan Hiwin linear rails — this combination matters because oscillating knife cutting involves rapid directional reversals at up to 1200 mm/s translational velocity, where rail straightness and servo response directly control whether nested patterns stay within tolerance over a full sheet. The 9 kW rated power covers the cutting head, vacuum pump and conveyor system running simultaneously, so buyers should confirm their facility can supply 380V ±10% on a dedicated circuit. HP-GL compatible control format means the system accepts files from common nesting software, but file format compatibility should be verified against the buyer’s existing workflow before the order is confirmed. The CCD camera and panoramic recognition positioning allows printed contour cutting, which is essential for advertising and packaging applications where cut lines must follow registered print marks rather than vector paths alone.
When the Wrong Configuration Reaches Your Workshop
I remember a Turkish buyer who received a flatbed cutter configured for standard cotton fabric. His actual production material was six-layer composite automotive interior laminate. Every cutting parameter was wrong — depth, oscillation frequency, vacuum pressure. It took four full days of on-site adjustment to reach acceptable edge quality. The machine was not defective; it was specified for a material it would never cut in production. [NEED_CITE: consequences of incorrect tool head specification for composite materials]
Wrong tool head selection produces ragged edges on dense foam or crushes cellular structure in sponge materials. Insufficient vacuum zoning causes small gasket parts to lift and shift during the final passes, ruining a nested sheet that took minutes to lay up. Promised CCD contour recognition that cannot track printed marks at production speed forces operators to slow down or abandon automated registration entirely.
Why Production Managers Choose This Build
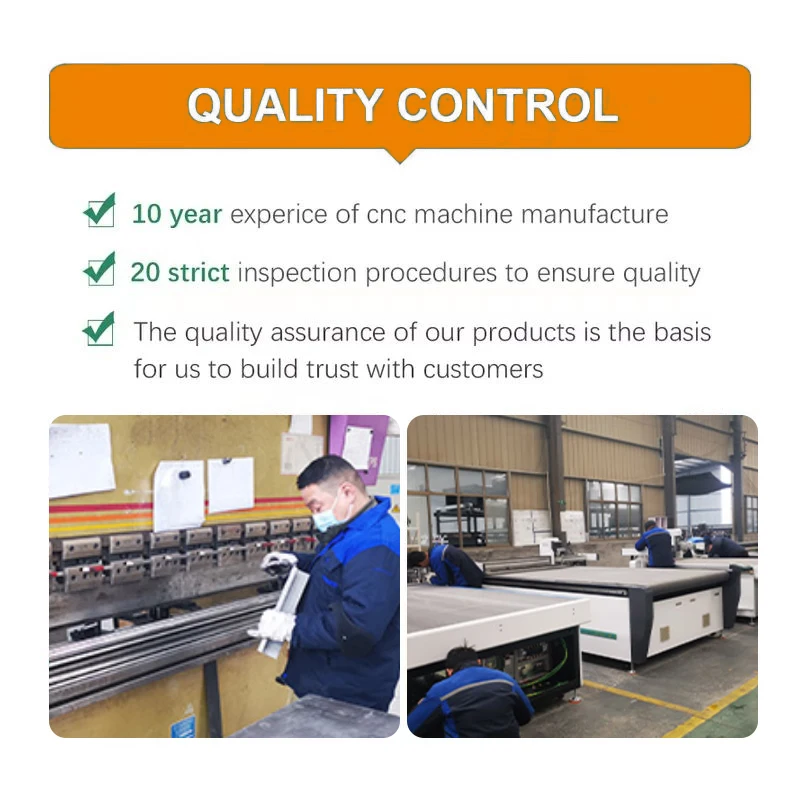
REALTOP designs and manufactures both knife and laser cutting systems under one roof, which means the RT-D2516/RT-S2516 was engineered specifically for flexible and semi-rigid non-metal materials where blade cutting produces clean, burr-free edges without thermal distortion. The tool head and table configuration are specified per material and production volume before the order is finalized, not selected from a default menu. CCD camera positioning is tested against the buyer’s actual printed material at production speed during the factory test phase. Software compatibility with the buyer’s nesting workflow is confirmed before shipment, eliminating the common discovery that exported DXF files lose layer information. Voltage, plug type and control language are documented and verified against target market requirements before the machine is crated.
Documentation & Verification
- Sample cutting report generated on the buyer’s own material, documenting tool head selection, cutting depth and edge quality results
- Tool head and table configuration list itemizing which knife type and vacuum zone layout is installed for the buyer’s material specification
- Electrical schematic with voltage confirmation sheet matching the target market’s supply standard
- Factory test record showing repeated accuracy and cutting performance across the full 1600×2500 mm working area
- Software licence and file format compatibility note confirming HP-GL workflow with the buyer’s nesting application
- Operation and maintenance manual with spare parts list in the buyer’s selected control language
Installation, Commissioning & Support
- Requires a level floor capable of supporting the 3450×2300 mm footprint plus operator clearance around all four sides of the RT-D2516/RT-S2516
- Dedicated 380V ±10% circuit needed for the 9 kW rated power draw, with plug type confirmed to local standard before shipment
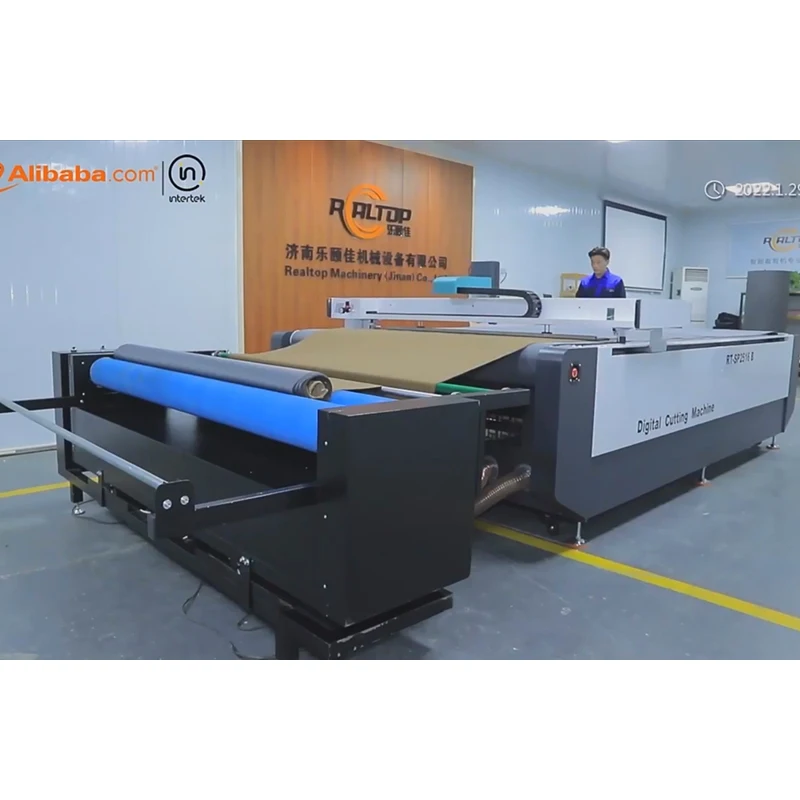
- Machine ships fully assembled — no on-site frame assembly required, reducing commissioning time to power connection and calibration
- First-run parameter tuning includes vacuum pressure adjustment, tool head zero-point setting and CCD camera mark registration on buyer’s material
- Operator training covers tool change procedures across the full head range from oscillating knife to creasing wheel
- Spare parts list identifies consumable blades, vacuum pump filters and belt segments for routine maintenance intervals
What We Need to Quote the Right Configuration
To recommend the correct tool head, vacuum zoning and conveyor setup for the RT-D2516/RT-S2516, we need the material type, maximum thickness and typical sheet dimensions from your production line. Tell us your daily cutting volume and whether your workflow relies on printed contour registration or pure vector cutting. Confirm your facility voltage, frequency and preferred control language so these are built into the machine from day one.
Frequently Asked Questions
Q: How is the tool head selected for my specific material and thickness?
A: We test-cut your actual material at our factory before finalizing the order. The sample report documents which knife type — oscillating, drag, circular or pneumatic — delivers acceptable edge quality at your required thickness. The tool head configuration is then locked into your order documentation, so the machine arrives with the right tools installed rather than a generic default set that requires weeks of trial and error on your production floor.
Q: What voltage and control language options are available for my market?
A: The RT-D2516/RT-S2516 is configurable for 380V ±10% supply with plug type matched to your local standard. Control language options include English, Russian, Italian and Chinese, with special languages available on request. We document the exact voltage, frequency, plug type and language in the specification confirmation before production begins, eliminating mismatches that would otherwise surface only when the machine is powered on at your facility.
Q: How is CCD contour recognition tested at production speed before shipment?
A: During the factory test phase, we run the buyer’s printed material through the CCD camera mark point positioning and panoramic recognition system at full translational velocity. The test verifies that the camera tracks registered marks without losing position across the entire 1600×2500 mm bed. Results are recorded in the factory test report, which ships with the machine so you have a documented baseline for your own calibration checks after installation.
Q: Can I send my material for sample cutting before placing the order?
A: Yes — sample cutting on the buyer’s own material is a mandatory step in our sales process. We run your actual production material, test multiple tool head configurations and cutting depths, then deliver a written sample report covering edge quality, cutting speed and recommended vacuum settings. This report forms the basis of your order specification and ensures the machine is built around your material, not a generic catalog configuration.
Q: What OEM and custom configuration options does the factory offer?
A: Beyond the standard tool head range, the RT-D2516/RT-S2516 accepts custom vacuum table zoning layouts, specialized conveyor belt specifications and non-standard working area adaptations. Panasonic servo motors can replace the standard Delta units. Control system language, software integration protocols and safety device configurations are all adjustable. Each custom requirement is documented in the tool head and table configuration list that accompanies the final quotation.
You may also like







商品评价
Clear filtersThere are no reviews yet.