



-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

In-House Design & Build — Every RT-D2516/RT-S2516 is configured from frame to tool head by the same team that assembled it, ensuring design intent matches factory output.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
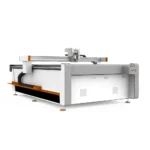
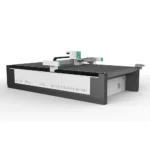
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600×2500 mm |
| Overall Dimensions | 3450×2300×1250 mm |
| Rated Power | 9 kW |
| Voltage | 380V ±10% |
| Cutting Thickness | ≤100 mm (varies with material) |
| Translational Velocity | 800–2000 mm/s |
| Repeatability | ≤0.1 mm |
| Servo Motor | Delta (optional Panasonic, availability to be confirmed per order) |
| Linear Rail | Taiwan Hiwin |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Working Table | Magnesium-aluminum alloy vacuum adsorption table (PVDF powder spraying, anodic oxidation, hard oxidation) |
| Vacuum Pump | 7.5 kW, integrated aviation aluminum shell with built-in silencer sponge |
| Conveyor Belt | Germany imported (basis not stated in source) |
| Tool Head Options | Swiss imported knife (vibration full/half cutting, cursor location), oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V cutting knife, drag knife, creasing wheel, dotted line knife, punching, brush |
| Visual Positioning Options | Small CCD camera mark point positioning, panoramic camera recognition positioning, projection positioning |
| Auto Feeding | Equipped |
| Safety Devices | Infrared induction blocking, anti-collision sensors on both sides of beam, emergency stop button |
| Instruction System | HP-GL compatible format |
| Standards | CE declared |
Application Suitability
| Application | Material or Output |
|---|---|
| Foam and composite panel cutting | High-density rubber, PE foam, EVA, sponge composite leather |
| Automotive interior components | Instrument panel skins, door panel fabric, headliner material, gasket sheets |
| Automotive sealing gasket production | Closed-cell foam, EPDM, silicone rubber sheets up to rated thickness |
| Footwear and bag component nesting | PU leather, genuine leather, textile laminates, synthetic uppers |
| Flexible industrial material processing | PVC sheets, soft glass, silicon pads, rubber compounds |
Why Specified Working Area Alone Leads to Cutting Failure on Composites
A cutting table is only as capable as the tool head and vacuum zoning matched to the actual material — not the brochure dimensions.
Buyers often specify a CNC oscillating knife cutting machine factory by working area alone, then discover the configured tool head cannot penetrate the material thickness they run daily. I saw this firsthand when a gasket manufacturer ordered based on table size, then switched to a denser rubber compound in production — the knife stalled mid-cut, and an entire batch was scrapped. The vacuum table zoning also matters: small gasket profiles lift off poorly partitioned zones, producing ragged edges and dimensional drift [NEED_CITE: vacuum adsorption zoning requirements for small-part CNC knife cutting].
Frame Rigidity and Long-Term Precision Under Oscillating Loads
The RT-D2516/RT-S2516 frame is built from an overall welded thick-wall seamless steel structure, heat-treated through high-temperature tempering and then finish-machined on a CNC machining center. This sequence relieves welding stress before the final pass, so the bed stays flat under continuous oscillating forces. When the high-power vibrating knife head drives into dense composite stock at rated translational velocity, frame deflection is what separates clean edges from tapered cuts.
Magnesium-Aluminum Vacuum Table and Zoning Strategy
The working surface uses a magnesium-aluminum alloy base treated with fluorocarbon PVDF powder spraying, anodic oxidation, and hard oxidation in sequence. This multi-layer finish resists scoring from drag knife and creasing wheel passes while maintaining flatness. The 7.5 kW vacuum pump with integrated silencer sponge provides sustained suction across the 1600×2500 mm area, and zoning configuration is specified per the buyer’s typical part geometry before the table is drilled.
Decoding the Specs That Matter in Composite Cutting
Cutting thickness rated at ≤100 mm is a ceiling that shifts with material density — closed-cell EVA foam at full depth behaves very differently from high-density EPDM rubber of the same thickness. The Swiss imported knife head supports vibration full cutting, half cutting, and cursor location, which allows kiss-cutting a composite skin without scoring the backing layer. Repeatability at ≤0.1 mm across the full working area depends on the Taiwan Hiwin linear rails and ball screw transmission working together; any play in either component multiplies at the far end of a 2500 mm stroke. The HP-GL instruction system compatibility matters when a buyer’s existing nesting software outputs directly to that format, avoiding a forced software migration [NEED_CITE: HP-GL compatibility in industrial CNC cutting workflows]. Servo selection between Delta and optional Panasonic affects acceleration curves on intricate contour paths — the choice should be confirmed against the buyer’s typical cut geometry.
What a Misconfigured Tool Head Costs Beyond the First Scrap Batch
Selecting an oscillating knife for a material that needs a high-power vibrating knife produces crushed foam cores and delaminated composite layers. I have watched a pneumatic knife drag through multi-layer foam because the air pressure was set for single-ply leather. Small parts cut on a vacuum table without adequate zoning lift at the trailing edge, shifting position and producing nested waste that jams the auto-feeding system. These failures do not show up in a specification sheet — they appear on the shop floor during the first full production run [NEED_CITE: tool head selection criteria for oscillating knife cutting on multi-density materials].
What This Purchase Channel Provides Before Shipment
Tool head and table configuration are specified per the buyer’s actual material and daily volume, not selected from a default catalog page. An in-house design team covers both knife and laser cutting technologies, so the cutting method matches the material rather than forcing one method across every substrate. CCD camera positioning is confirmed against the buyer’s printed mark style and production speed before the vision system is mounted. Software file format compatibility — particularly HP-GL import and nesting workflow integration — is verified before the order is locked. Voltage, plug type, and control panel language are confirmed in writing before the machine enters final assembly, not discovered at the destination port [NEED_CITE: voltage and plug standard variations across export markets for CNC machinery].
Documentation & Verification
- Machine specification sheet locking tool head, vacuum zoning, and voltage per your order
- Factory test record showing sample cuts on your submitted composite material before dispatch
- Electrical schematic with 380V ±10% confirmation matching your facility supply
- Software licence and HP-GL file format compatibility note delivered with the control system
- Spare parts list covering Swiss knife blades, vacuum table seals, and conveyor belt segments
- Packing photographs documenting machine condition before crate closure
Installation, Commissioning & Support
- Foundation must support the 3450×2300×1250 mm footprint with level tolerance across the full working table
- Dedicated 380V ±10% circuit rated for the 9 kW machine draw plus the 7.5 kW vacuum pump
- Machine ships with beam and table sections separated; on-site reassembly and rail alignment required
- First-power commissioning includes servo tuning, vacuum zone mapping, and test cuts on your material
- Operator training covers tool head changeover, CCD mark recognition setup, and HP-GL file loading
- Wear items including oscillating knife blades and vacuum seals stocked for multi-week lead times
Preparing a Configuration Inquiry
Send material type, density, and maximum thickness along with typical sheet dimensions and daily cut volume. Specify your facility voltage, frequency, and preferred control language. If your current workflow relies on specific nesting software, include a sample file so format compatibility can be verified before the CNC oscillating knife cutting machine factory confirms the build configuration.
Frequently Asked Questions
Q: How is the correct tool head selected for different composite densities?
A: Each material sample is test-cut using multiple head options — oscillating, pneumatic, or high-power vibrating — to evaluate edge quality and cutting depth. The selected head and its operating parameters are written into the specification sheet before production begins, so the configuration matches your actual stock rather than a generic recommendation.
Q: What can be customized for OEM or distributor orders?
A: Working area dimensions, voltage rating, plug type, control panel language, and software interface can all be configured to match the destination market. The CNC oscillating knife cutting machine factory documents each customization point in the order confirmation, and OEM branding options are discussed at the quotation stage with full factory test records provided before shipment.
Q: How does the sample cutting and factory visit process work?
A: Buyers send representative material rolls or sheets to the Jinan facility. The engineering team runs cutting tests across the thickness range and delivers a sample cutting report showing edge quality, achievable speed, and recommended tool head. Factory visits can be scheduled to observe the test run and review quality control checkpoints on the assembly line.
Q: What does on-site installation and training involve?
A: An engineer assembles the separated sections, aligns the Hiwin linear rails, calibrates the vacuum zones, and runs acceptance cuts on your material. Training covers tool head swap procedures, CCD camera calibration, and HP-GL file import. Travel and accommodation costs for the installation visit are clarified in the purchase agreement before dispatch.
Q: How are spare parts and consumables managed after delivery?
A: A spare parts list ships with the machine, identifying wear items such as oscillating knife blades, vacuum table seals, and conveyor belt segments. The factory maintains stock of standard consumables, and orders are fulfilled based on current availability with typical multi-week lead times for international shipping.
You may also like







商品评价
Clear filtersThere are no reviews yet.