


-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

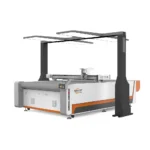
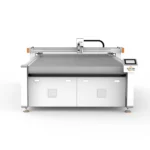
In-House Design & Build — tool head and vacuum table configured per leather grade and production volume before the order is placed.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | Realtop-2516 |
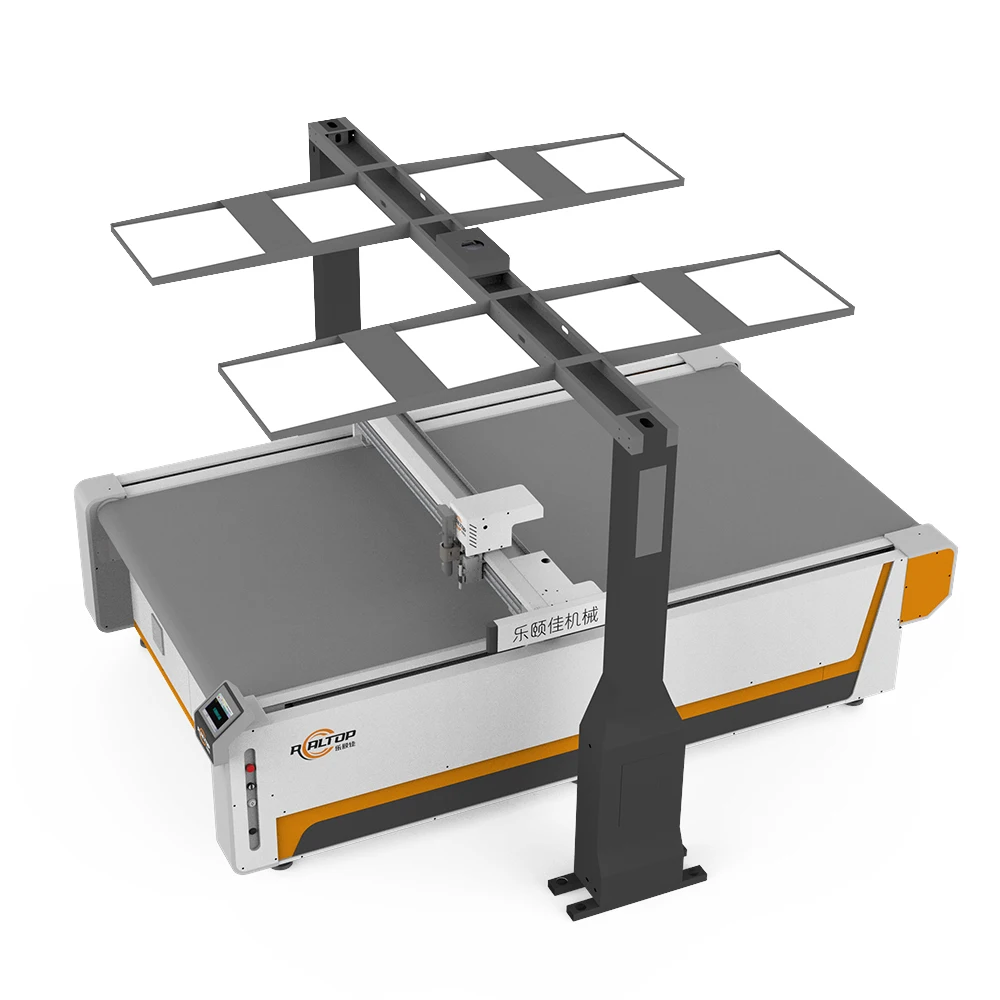
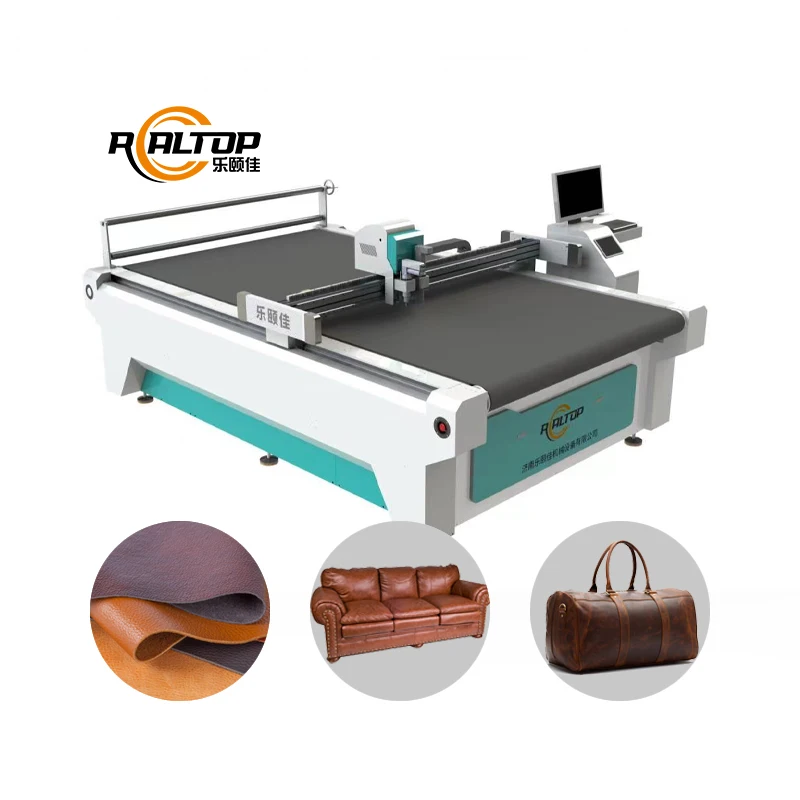
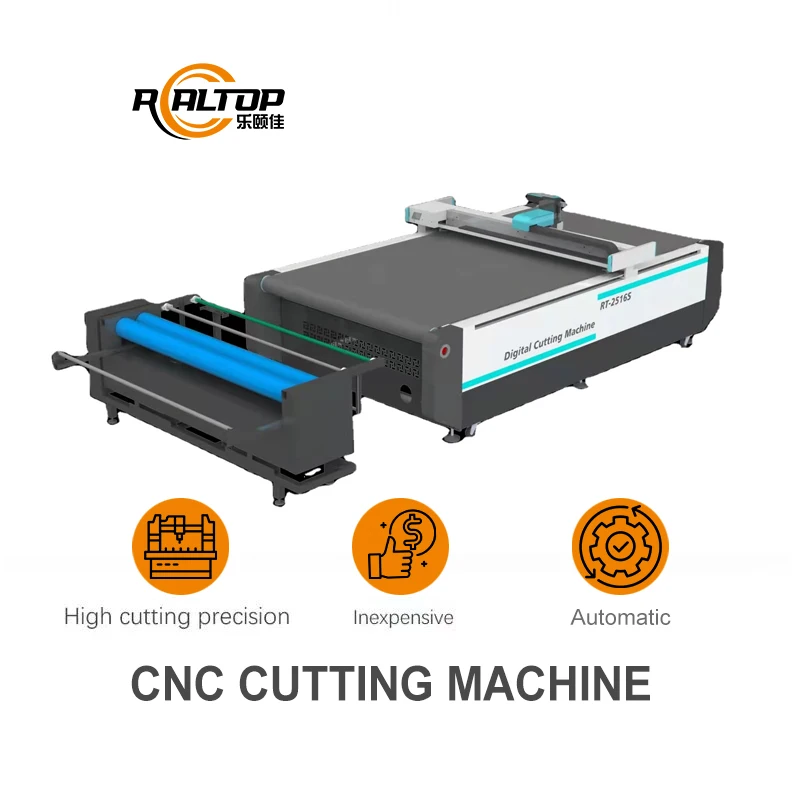
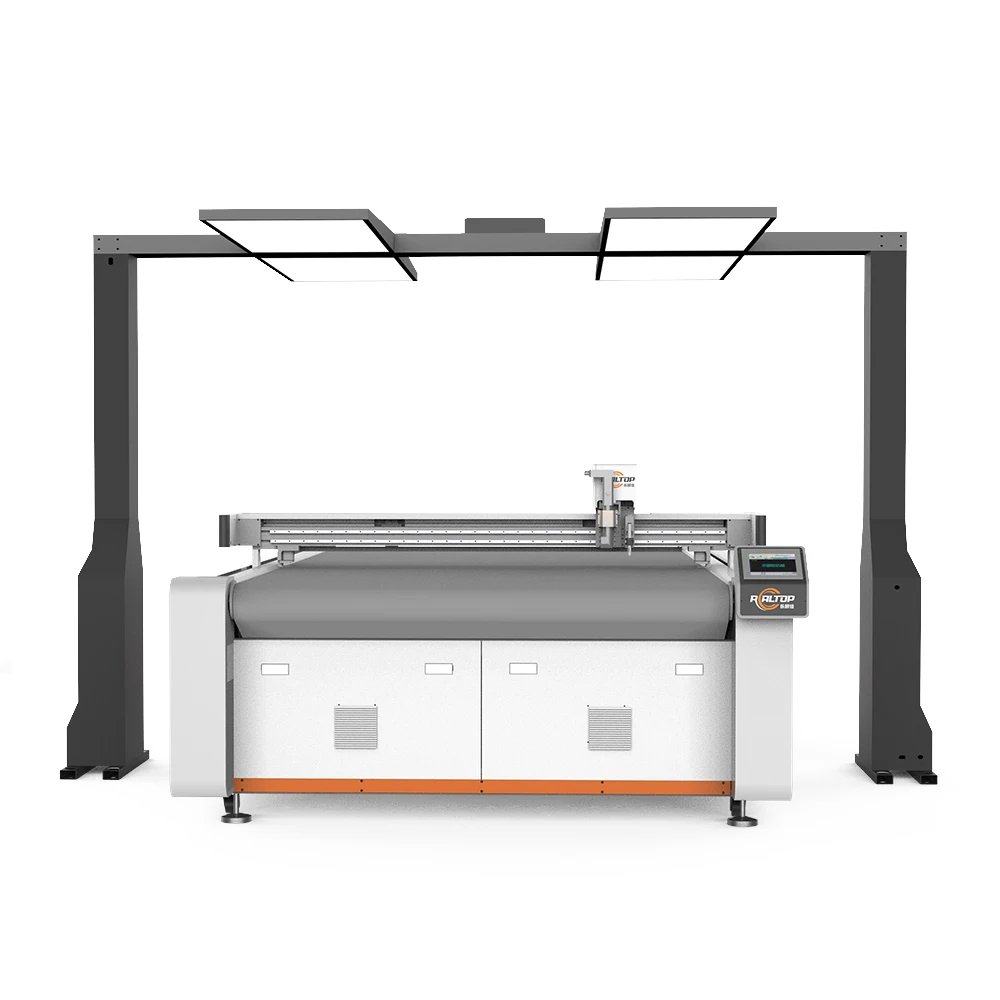
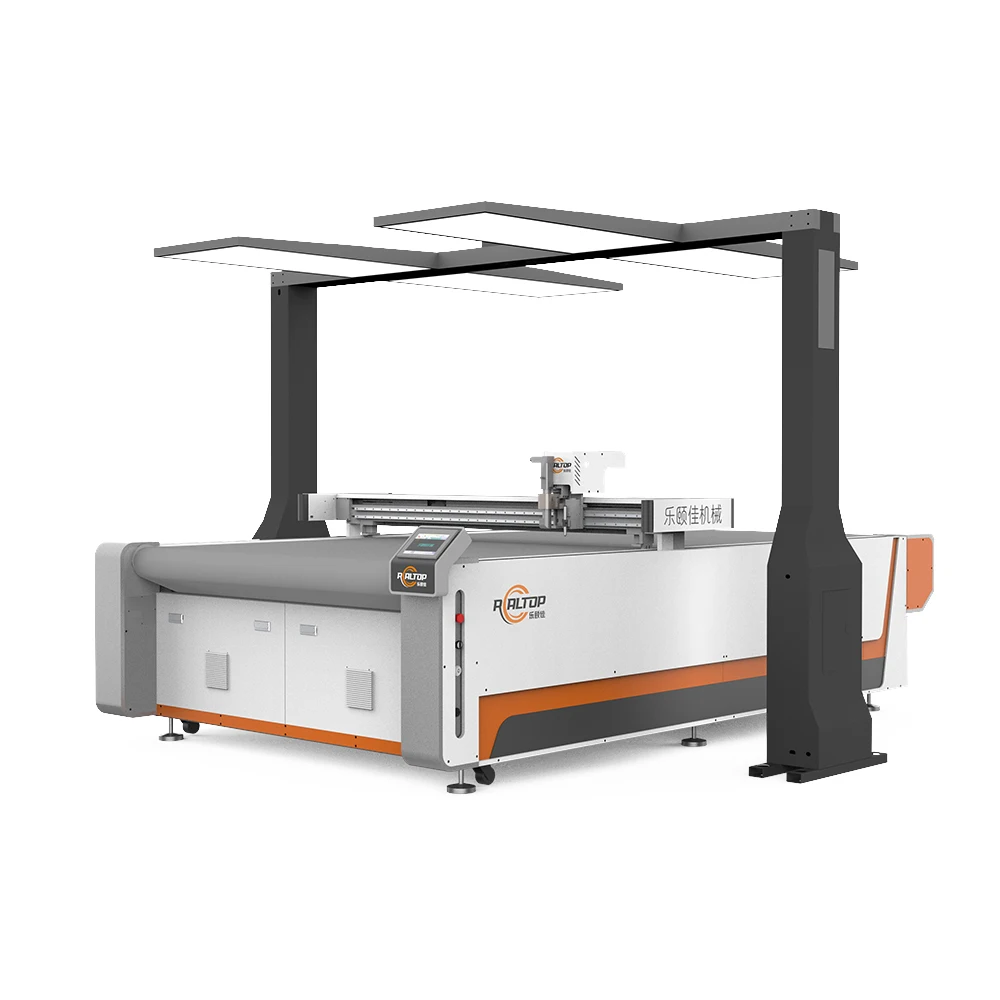
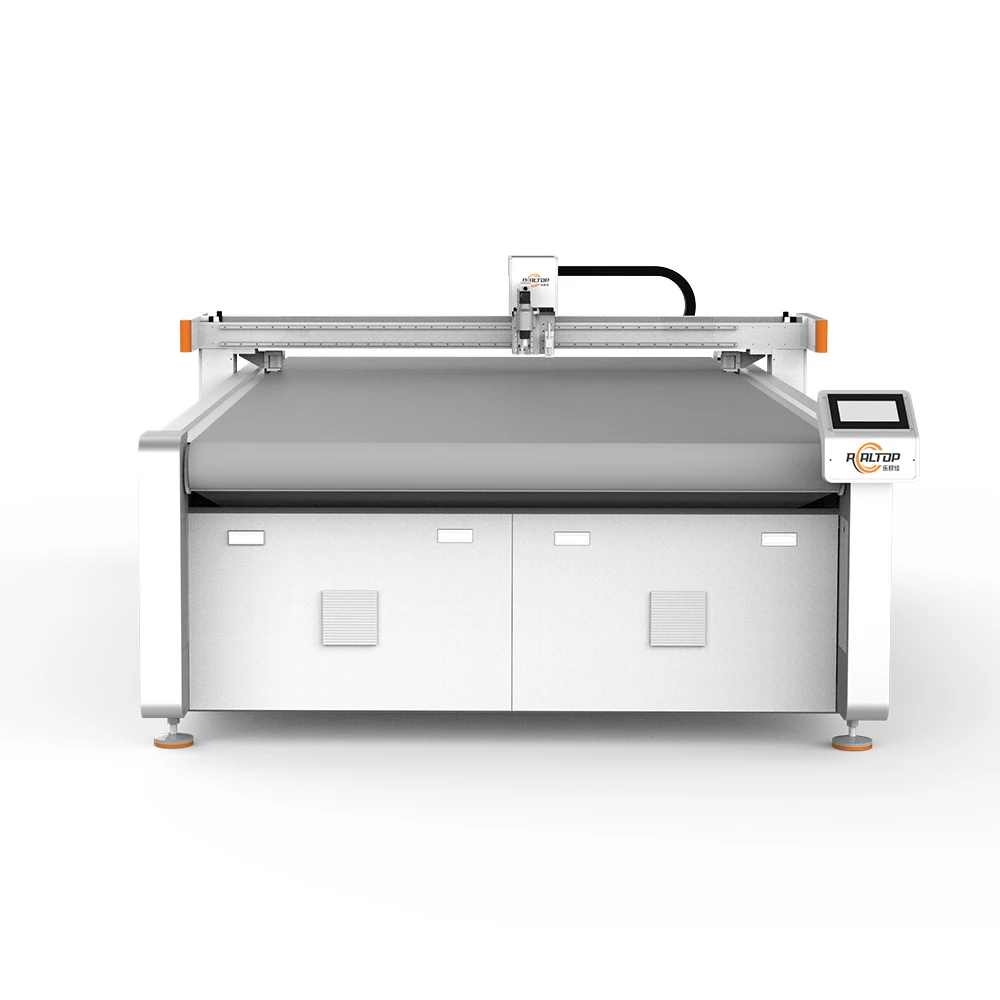
| Product Type | CNC Oscillating Knife Leather Cutting Machine |
| Cutting Area | 1600 × 2500 mm |
| Cutting Thickness | ≤ 30 mm |
| Cutting Speed | 0–2000 mm/s (basis not stated in source) |
| Cutting Accuracy | ±0.1 mm |
| Tool Options | Oscillating knife, Driven rotary knife, Pneumatic knife, Creasing wheel, Kiss cutting tool, Milling tool, V-groove knife |
| Vacuum Pump | 9 kW |
| Vacuum Table | Aluminum bellows vacuum table with high flatness |
| Machine Frame | Heavy-duty frame with precision-ground surface |
| Servo Motors | Multiple servo drive options available including Panasonic, Delta, and Dorna (source value — verify against manufacturer catalog) |
| Control Panel | PLC control panel with intuitive interface |
| Language Options | English, Russian, Italian, Chinese, etc. (Special languages can be customized) |
| Voltage | 110V, 220V, 380V (basis not stated in source — confirm frequency and phase) |
| Profile Format | PLT, DXF, AI, PDF |
| Safety Device | Infrared sensor device and emergency stop device |
| Machine Size | 3300 × 2100 × 1350 mm |
| Certification | CE (from certifications section image, specific standards not detailed in text) |
Application Suitability
| Application | Material or Output |
|---|---|
| Footwear and leather goods | Genuine and synthetic leather for shoe uppers, bags, belts, and wallets |
| Automotive interiors | Leather seat covers, car mats, and interior trim components |
| Apparel and textile | Patterned fabrics, composite materials, and sofa upholstery |
| Advertising and packaging | Foam boards, PVC sheets, adhesive stickers, and carton samples |
What a Cutting Area Figure Leaves Out for Leather
A 1600×2500 mm bed only matters if the tool head and vacuum zoning match your leather thickness and part geometry.
Many buyers focus on working area and overlook the cutting method. When a machine specified on bed size alone meets thick, uneven genuine leather, the result is ragged edges and crushed grain. A CNC Leather Cutting Machine manufacturer that does not test on your actual material cannot guarantee edge quality or contour accuracy across a full shift. The tool head, vacuum hold-down, and blade oscillation frequency all change depending on whether you run 1.2 mm garment leather or 4 mm sole stock [NEED_CITE: CNC knife cutting parameters for varying leather densities].
Tool Head Selection Across Leather Types
The Realtop-2516 supports interchangeable tool heads including oscillating knife, driven rotary knife, and pneumatic knife. Each serves a different leather cutting task. An oscillating knife handles most garment and upholstery leathers cleanly, while a driven rotary knife suits thicker hides and long straight cuts where edge compression must be avoided. The CNC Leather Cutting Machine manufacturer configures the tool head based on sample cuts run on your actual material before the build is finalized.
CCD Contour Recognition and Genuine Leather Nesting
Genuine leather arrives in irregular shapes with natural defects. The CCD camera contour recognition system reads the hide outline and detects grain patterns or printed marks, allowing the nesting software to place pattern pieces around scars and thin spots. This reduces manual alignment and improves hide utilization. For leather goods producers running premium hides, defect-aware nesting directly affects material cost per cut piece [NEED_CITE: material yield optimization in genuine leather cutting].
Reading the Specs That Matter for Leather Production
The 9 kW vacuum pump paired with an aluminum bellows table provides even adsorption across the full 1600×2500 mm surface. For small leather parts like belt loops or shoe tongue pieces, vacuum zoning prevents lift during high-speed oscillation. Cutting accuracy of ±0.1 mm keeps nested pieces consistent across a full hide. The PLC control panel supports multiple display languages, reducing operator error when production teams work in non-English environments. Servo motor options span several brands, and the choice affects acceleration behavior on intricate contours. Profile format compatibility with PLT, DXF, AI, and PDF means your existing design files load without conversion steps that can distort curves.
The Hidden Cost of Skipping the Sample Cut
When a leather cutting machine arrives without a prior sample test on your hide stock, problems surface during the first production run. Edges may show micro-tears on the grain side, or the vacuum table may fail to hold small pattern pieces flat at full cutting speed. Correcting these issues on-site means waiting for replacement blades, reconfigured vacuum zones, or software parameter adjustments — all while production sits idle [NEED_CITE: common causes of CNC knife cutting defects in natural leather].
Why Source This Build Directly
The design team engineers both knife and laser platforms in-house, so leather buyers get the cutting method matched to their material rather than a forced solution. Tool head and table configuration are specified per hide thickness and daily volume before the order is locked. CCD camera positioning is validated on your printed or grained leather during the sample phase. Software compatibility with your nesting workflow is confirmed before production begins. Voltage, plug type, and control language are set to your facility requirements and documented before the machine leaves the factory floor.
Documentation & Verification
- Machine specification sheet listing your confirmed tool head and vacuum table configuration
- Sample cutting report on your leather stock showing edge quality and contour accuracy
- Electrical schematic with voltage, phase, and frequency matched to your market
- Factory test record documenting full-bed cutting performance before crating
- Software licence and file format compatibility note for your nesting workflow
- Spare parts list covering blades, oscillation blocks, and vacuum seals
Installation, Commissioning & Support
- Heavy-duty frame requires a level concrete floor within the 3300×2100 mm footprint clearance zone
- 9 kW vacuum pump and servo drives require a dedicated circuit matching your confirmed voltage and phase
- Machine ships partially assembled; table leveling and gantry alignment completed on-site
- First-run parameter tuning covers blade depth, oscillation frequency, and vacuum zoning for your leather type
- Operator training covers PLC interface navigation in your selected language and tool head changeover procedure
- Spare blade and oscillation block kit included for initial production weeks
What to Prepare Before Your Inquiry
Send your leather type, typical thickness range, and the largest hide or sheet size you process. Include your daily cutting volume and the part geometries you run most often. Specify your facility voltage, frequency, and preferred control language. If you have an existing nesting software or file format workflow, note that so compatibility can be confirmed before the build.
Frequently Asked Questions
Q: How is the tool head selected for different leather types and thicknesses?
A: Tool head selection depends on leather density, thickness, and the edge quality your product requires. Oscillating knives suit most garment and upholstery leathers, while driven rotary knives handle thicker hides where edge compression must be minimized. The final choice is validated through sample cuts on your actual material before the machine build is finalized.
Q: Can the machine handle genuine leather contour recognition at production speed?
A: The CCD camera system reads hide outlines and detects natural defects or printed grain marks. Nesting software places pattern pieces around irregularities to maximize hide utilization. Recognition speed depends on mark contrast and lighting conditions, which are tested on your leather stock during the sample phase to confirm reliable tracking.
Q: What voltage and control language options are confirmed before shipment?
A: Voltage options include 110V, 220V, and 380V configurations, with frequency and phase confirmed for your market before production. The PLC control panel supports English, Russian, Italian, Chinese, and other languages on request. Both specifications are documented in the electrical schematic provided before the machine ships.
Q: How is vacuum zoning configured for small leather parts?
A: The aluminum bellows vacuum table is divided into zones that can be activated independently. For small parts like belt loops or shoe components, targeted zoning concentrates hold-down force where pieces are being cut, preventing lift during high-speed oscillation. Zone layout is configured based on your typical part geometry and nesting pattern.
You may also like







商品评价
Clear filtersThere are no reviews yet.