





-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

In-House Build Chain — Every frame is welded from thick-walled seamless steel, high-temperature tempered, and finished on a CNC machining center before assembly begins.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | RT-D2516/RT-S2516 |
| Product Type | CNC Oscillating Knife Cutting Machine |
| Working Area | 1600×2500 mm |
| Machine Size | 3450×2300×1250 mm |
| Rated Power | 9 kW |
| Translational Velocity | 800–1200 mm/s |
| Cutting Speed | 200–800 mm/s (depending on material type and thickness) |
| Repeated Accuracy | ≤0.1 mm |
| Voltage | 380V±10% |
| Table Type | Magnesium-aluminum alloy vacuum surface with PVDF spray, anodic and hard oxidation |
| Vacuum Pump | 7.5 kW, integrated aviation aluminum shell with built-in silencer |
| Transmission System | Digital servo motor, linear guide, synchronous belt, imported ball screw |
| Rail | Taiwan Hiwin |
| Safety Device | Infrared induction blocking, anti-collision, emergency stop |
| Auto Feeding | Yes |
| Conveyor Belt | Germany imported |
| Instruction System | HP-GL compatible format |
| Visual Positioning Options | Small CCD mark point, panoramic camera recognition, projection positioning |
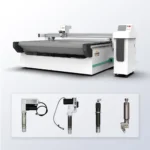
| Tool Head Options | Oscillating knife, pneumatic knife, high-power vibrating knife, circular knife, V-cutting, drag knife, creasing wheel, dotted line, punching, brush |
Application Suitability
| Application | Material or Output |
|---|---|
| Soft Home Furnishings & Automotive Interiors | Fabric, textile, leather, synthetic hide, composite upholstery layers |
| Packaging & Corrugated Box Sampling | Corrugated cardboard, plastic box, cardboard, EPE foam, sticker, film |
| Footwear, Bags & Luggage | Shoe material, luggage material, PU, EVA, non-woven fabric |
| Gasket & Sealing Fabrication | Rubber, sponge, PTFE, ETFE, sealing pads, fiberglass |
| Graphic Advertising & Signage | PVC, PP, PE, foam board, XPE, printed vinyl |
Why Machine Weight Matters Before the Spindle Starts
A rigid frame built in-house is the foundation of long-term cutting precision, preventing the vibration that ruins edge quality on multi-layer textiles.
When evaluating a CNC oscillating knife cutting machine manufacturer, buyers often focus on travel speed and software features while treating the frame as an afterthought. The reality is that a chassis constructed from thin, un-tempered steel will absorb high-frequency vibration from the oscillating head. Over time, this translates to micro-movements in the gantry, causing ragged edges on delicate fabrics or dimensional drift across a 2500 mm cutting bed [NEED_CITE: structural rigidity standards for CNC flatbed cutting tables].
I have walked into workshops where machines of this class were producing perfectly cut single-ply vinyl but failing completely on 15-layer composite automotive upholstery. The issue was not the knife, the vacuum, or the software. It was the frame flexing under the dynamic load of the high-power vibrating head at high translational speeds. A CNC oscillating knife cutting machine manufacturer that controls the welding, tempering, and CNC machining of its own frames can guarantee that the geometry measured on day one remains true years into production.
From Welding Bed to Machining Center
The frame of the RT-D2516/RT-S2516 begins as thick-walled seamless steel, not extruded aluminum or bolted modular sections. After the initial welding, the entire structure undergoes high-temperature tempering to relieve internal stresses induced by the heat of welding. This thermal cycle is critical; skipping it means the frame will slowly warp as ambient workshop temperatures fluctuate over the seasons.
Once tempered, the mounting surfaces for the linear rails and rack are finished on a large-format CNC machining center. This ensures the datum planes are perfectly coplanar. A CNC oscillating knife cutting machine manufacturer that relies on third-party welders often skips this step or outsources it, losing control over the final geometric tolerance.
The Table Surface and Flatness Tolerance
The working table uses a magnesium-aluminum alloy base, chosen for its strength-to-weight ratio and resistance to warping under continuous vacuum load. The surface then undergoes a multi-stage treatment: fluorocarbon PVDF powder spraying, followed by anodic oxidation and hard oxidation.
This is not a cosmetic finish. The hard oxidation layer provides a wear-resistant surface that prevents the knife tip from gouging the table during full-cut operations, while the PVDF layer reduces friction as the auto-feeding conveyor advances heavy material rolls. The 7.5 kW vacuum pump, housed in an aviation aluminum shell with integrated silencer sponge, pulls air through this precisely machined surface to hold materials flat without the localized lift that causes the knife to snag on small, intricate pattern pieces [NEED_CITE: vacuum adsorption zoning for small part retention].
How the Drive System Dictates Contour Accuracy
The transmission relies on a digital servo motor paired with imported ball screws and Taiwan Hiwin linear guides. For an oscillating knife cutting thick foam or multi-layer gasket material, the servo must make thousands of micro-corrections per second to maintain the cutting path.
The ≤0.1 mm repeated accuracy specification is only achievable because the synchronous belt and ball screw combination eliminates the backlash common in cheaper rack-and-pinion setups. When the tool head switches from a full-cut oscillating knife to a creasing wheel or a V-cutting knife mid-job, the drive system must reposition instantly without overshoot. This level of control is what separates a machine that can handle complex automotive interior patterns from one limited to simple straight-line signage cuts.
The Cost of Ignoring Tool Head Configuration
Selecting the wrong tool head for a specific material is a frequent source of post-delivery disputes. A buyer cutting XPE foam for packaging inserts who specifies only a standard drag knife will experience crushed edges and excessive dust generation, as the drag knife drags through the foam rather than slicing it. Conversely, using a high-power vibrating knife on thin, printed vinyl without the correct CCD mark point positioning will result in contour misalignment, wasting entire sheets of pre-printed material.
A CNC oscillating knife cutting machine manufacturer must map the buyer’s exact material stack to the correct tool head—oscillating, pneumatic, circular, or punch—before the machine leaves the factory. The cost of retro-fitting a new tool carriage and recalibrating the Z-axis in the field far exceeds the cost of specifying it correctly during the initial build [NEED_CITE: tool head selection matrix for non-metal cutting].
Why Procurement Should Start at the Factory Gate
Sourcing directly from the manufacturing floor eliminates the specification drift that occurs when machines pass through multiple trading layers. The in-house design team configures the RT-D2516/RT-S2516 based on the buyer’s material thickness, daily volume, and factory footprint.
Because the core factory controls the build from frame welding to final assembly, OEM branding, custom voltage configurations (such as adapting the 380V±10% system to local grid requirements), and localized control language interfaces are integrated during production, not hacked together post-shipment. Every unit undergoes a full factory test using the buyer’s actual material sample before it is cleared for crating, ensuring the machine’s capabilities match the production reality.
Documentation & Verification
- Factory test record confirming cutting accuracy on buyer-supplied fabric and foam samples.
- Electrical schematic and voltage confirmation sheet matching target facility power grid.
- Tool head and vacuum table zoning configuration list matched to specific material types.
- Operation and maintenance manual with localized control language and HP-GL format notes.
- Spare parts list including Swiss imported knife consumables and Germany imported conveyor belt segments.
- CE declaration documentation for applicable export market machinery directives.
Installation, Commissioning & Support
- Foundation must be level concrete capable of supporting the 3450×2300×1250 mm machine footprint and dynamic cutting loads.
- Dedicated 380V±10% circuit required for the 9 kW main system and separate line for the 7.5 kW vacuum pump.
- Gantry and tool head carriage are assembled on-site and laser-aligned to the pre-machined table datum.
- First-run commissioning includes calibrating the Delta servo motors and verifying the ≤0.1 mm repeated accuracy.
- Operator training covers auto-feeding setup, CCD panoramic camera mark point positioning, and tool head changeover procedures.
- Preventative maintenance schedule provided for Hiwin rail lubrication and synchronous belt tension checks.
Preparing the Technical Inquiry
To ensure the RT-D2516/RT-S2516 is configured for your specific production environment, please provide the exact material types, maximum thickness, and the largest sheet dimension you intend to process. Detail your local voltage and frequency standards, and specify any required OEM branding or localized software language preferences for the control interface.
Frequently Asked Questions
Q: How does the factory ensure frame precision from welding through to final assembly?
A: The frame is constructed from thick-walled seamless steel and undergoes high-temperature tempering to relieve internal stress. The mounting surfaces are then finished on a CNC machining center to guarantee coplanarity, ensuring the Taiwan Hiwin rails track true across the entire 1600×2500 mm working area without deflection.
Q: Can the machine be customized for different local power grids and control languages?
A: Yes. While the standard rated power is 9 kW at 380V±10%, the electrical system can be configured during assembly to match specific regional voltage and frequency requirements. The instruction system and control interface language are also customized and verified before the machine leaves the factory.
Q: What quality control steps are performed before the machine is shipped?
A: Every unit undergoes a comprehensive factory test using the buyer’s actual material samples. We verify the cutting speed, edge quality, and ≤0.1 mm repeated accuracy. The vacuum table zoning is tested under full load, and a formal test record along with the electrical schematic is shared with the buyer prior to dispatch.
Q: How is the vacuum table zoning configured for different part sizes?
A: The magnesium-aluminum alloy table is divided into specific vacuum zones. This allows the 7.5 kW pump to concentrate suction on the exact area where the material is being cut, preventing small pattern pieces from lifting or shifting during high-speed oscillating knife operations.
You may also like







商品评价
Clear filtersThere are no reviews yet.