


-
 Courier delivery
-
 DHL Courier delivery
-
 Warranty 1 year
-
 Free 30-Day returns

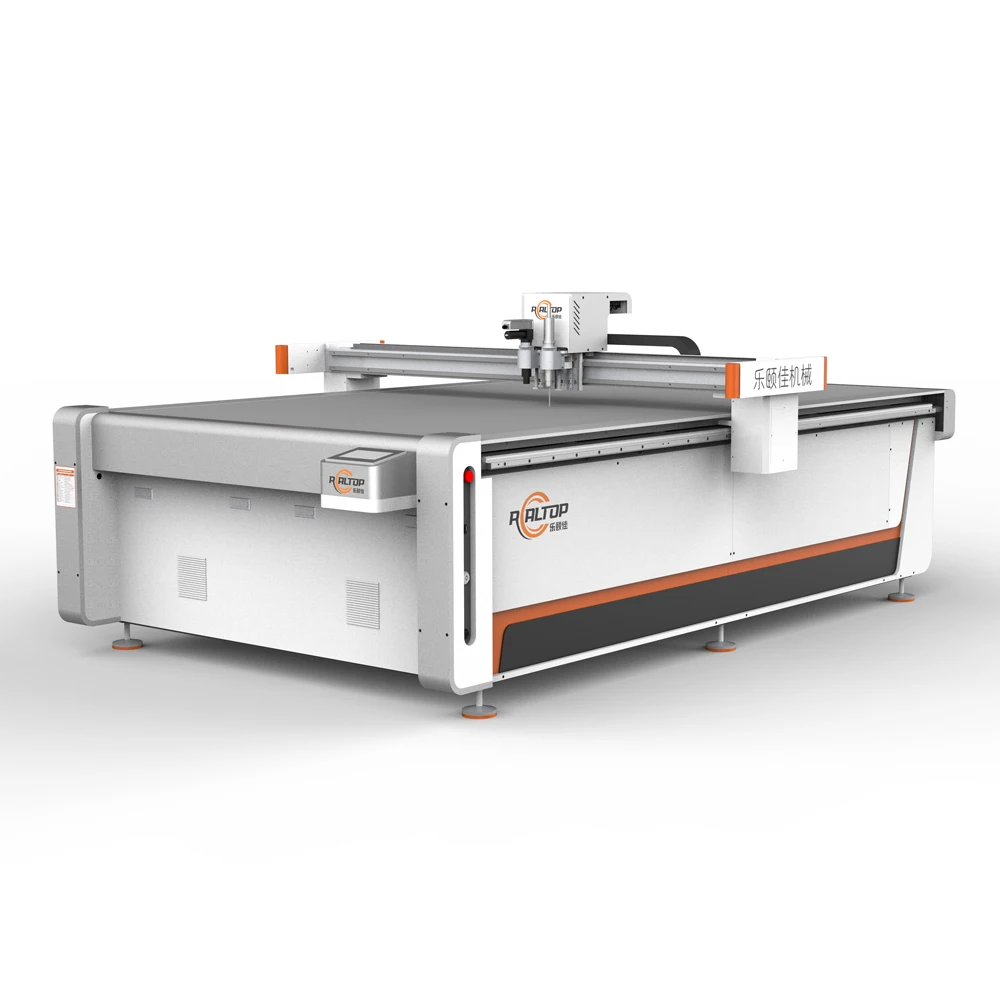
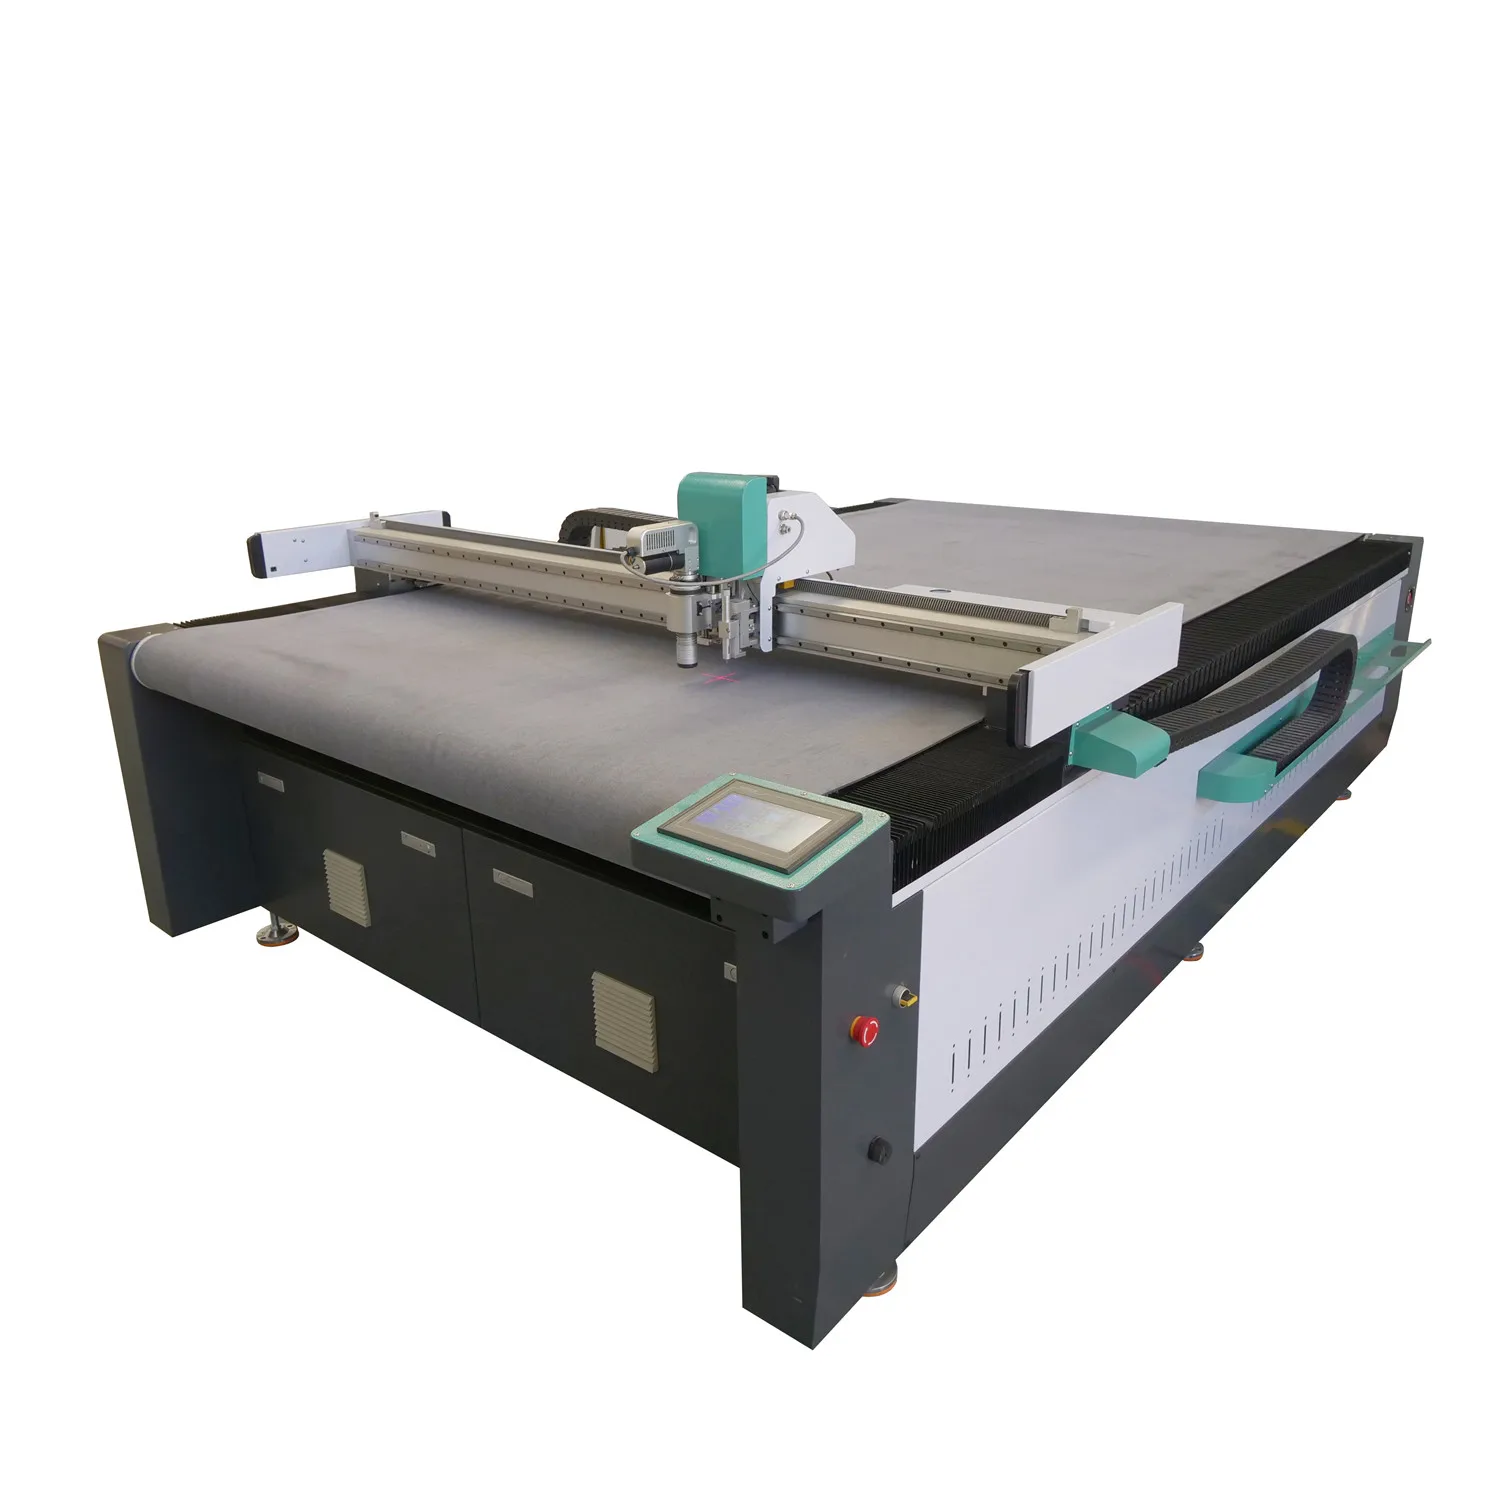
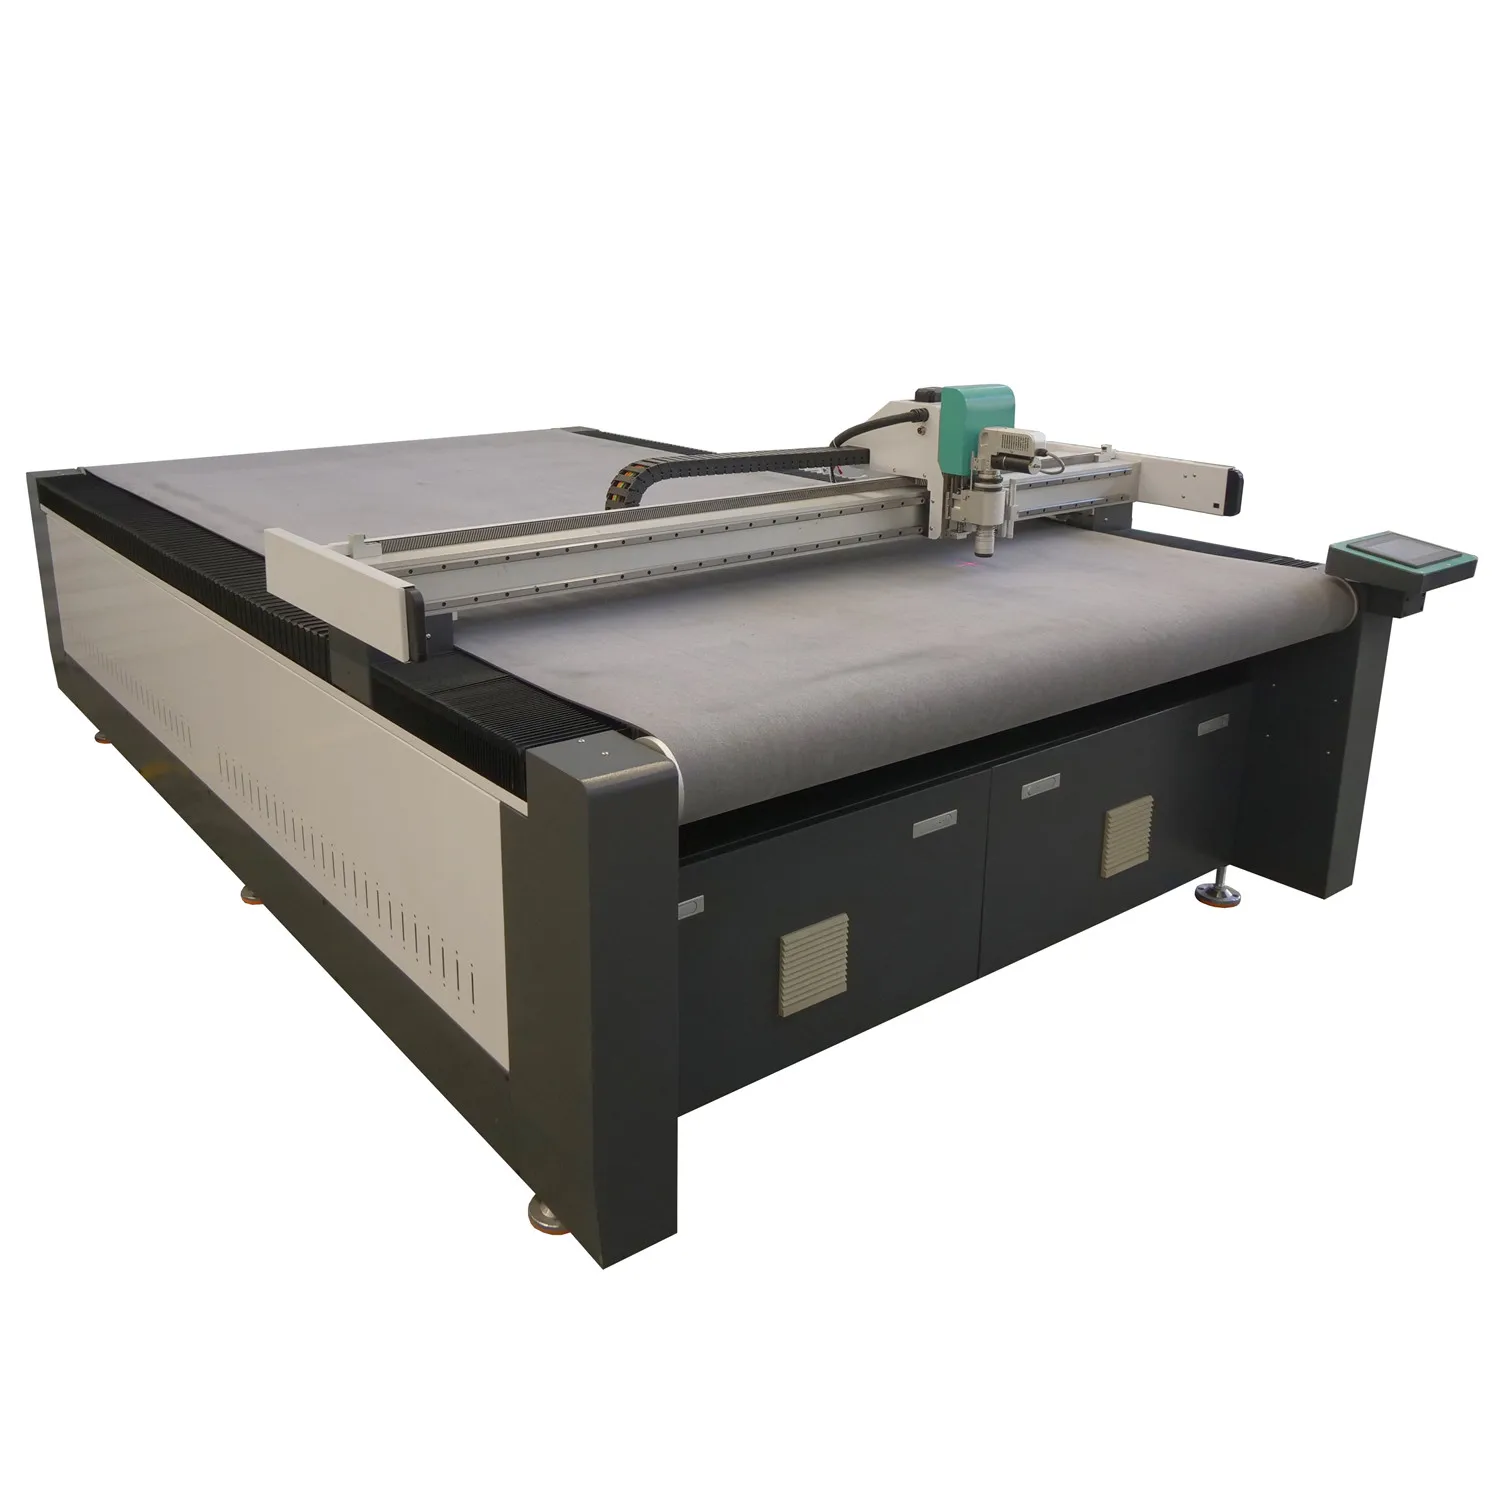
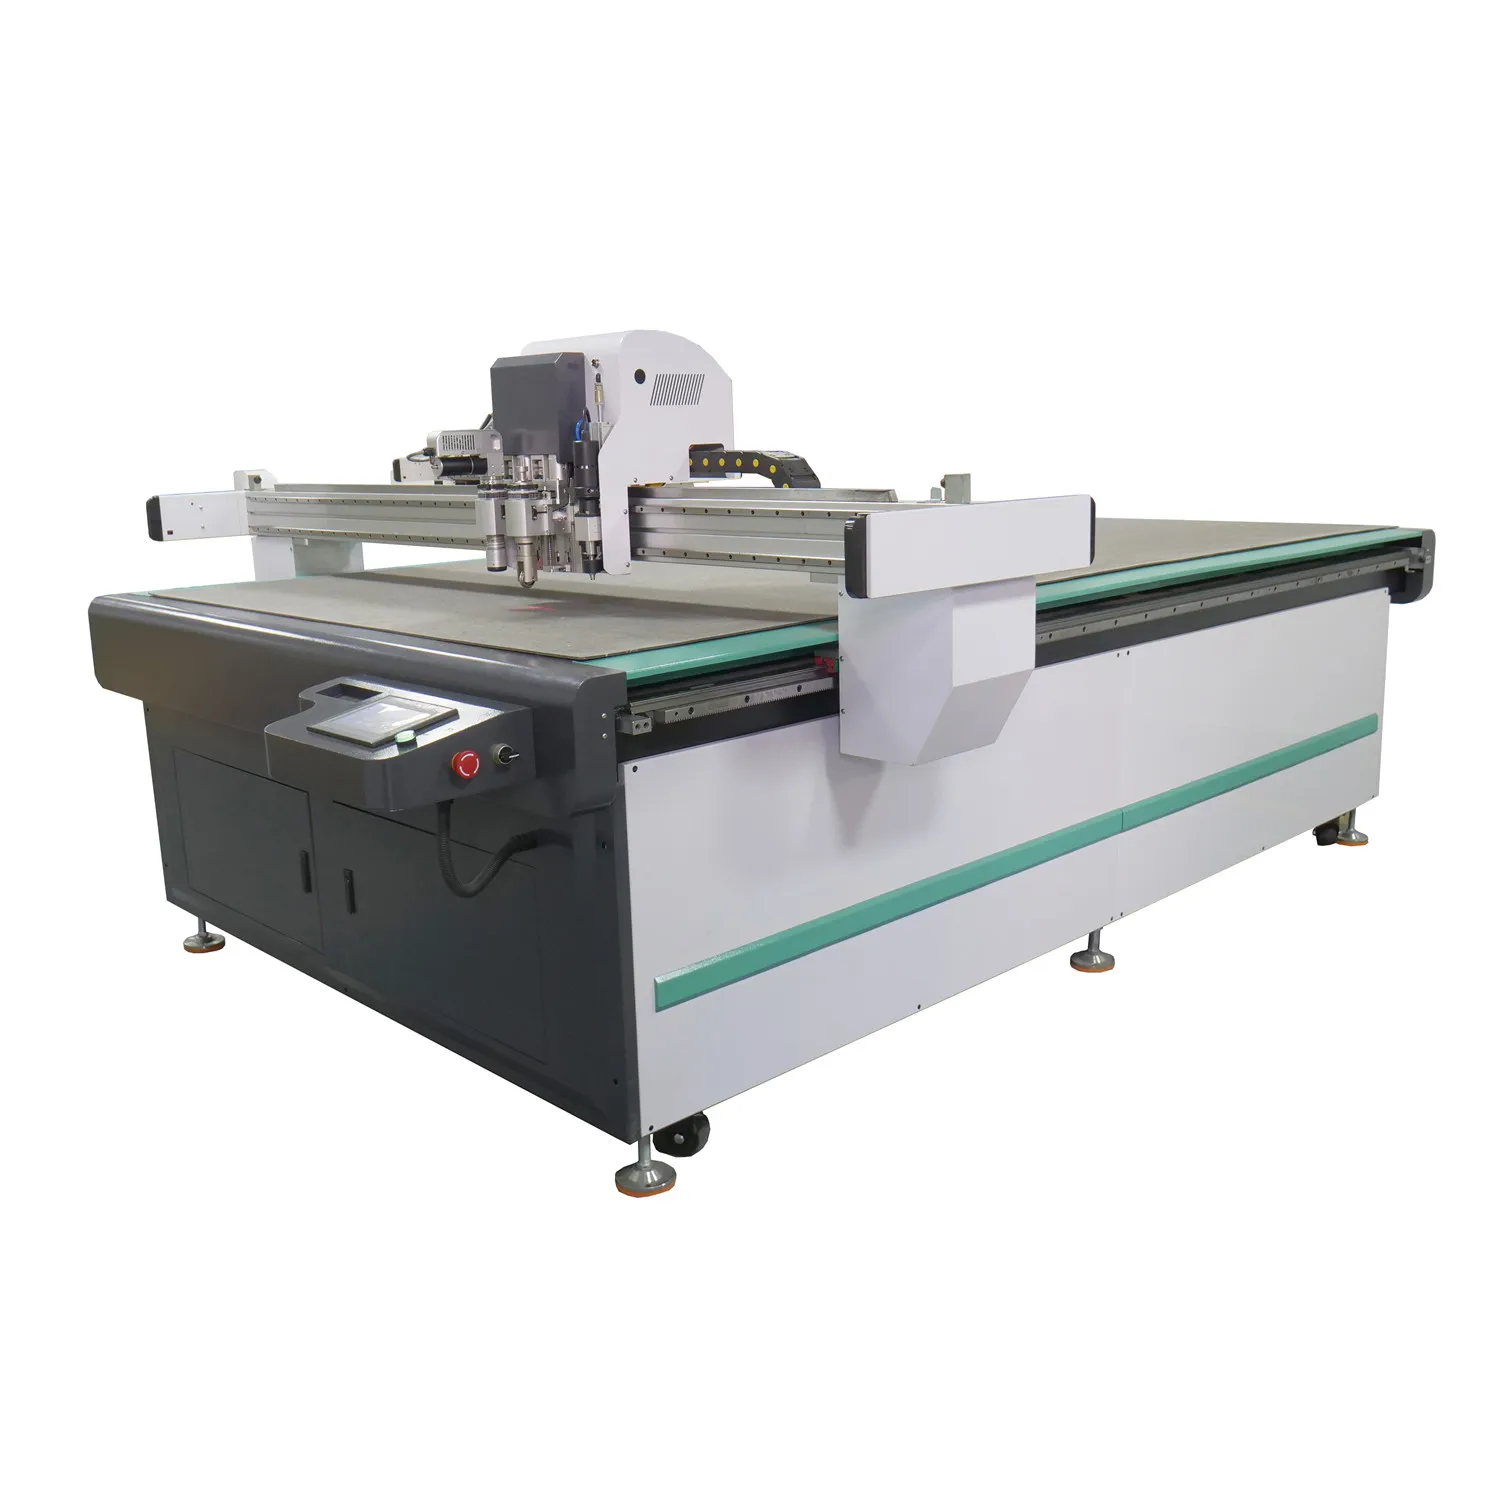
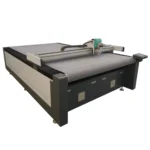
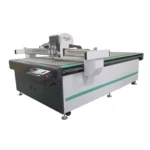
Precision Configuration — Realtop configures tool head type, vacuum table zoning, and electrical specifications per your leather thickness and local grid standard before the RT-D2516/RT-S2516 leaves the factory.
Technical Specifications
| Parameter | Value |
|---|---|
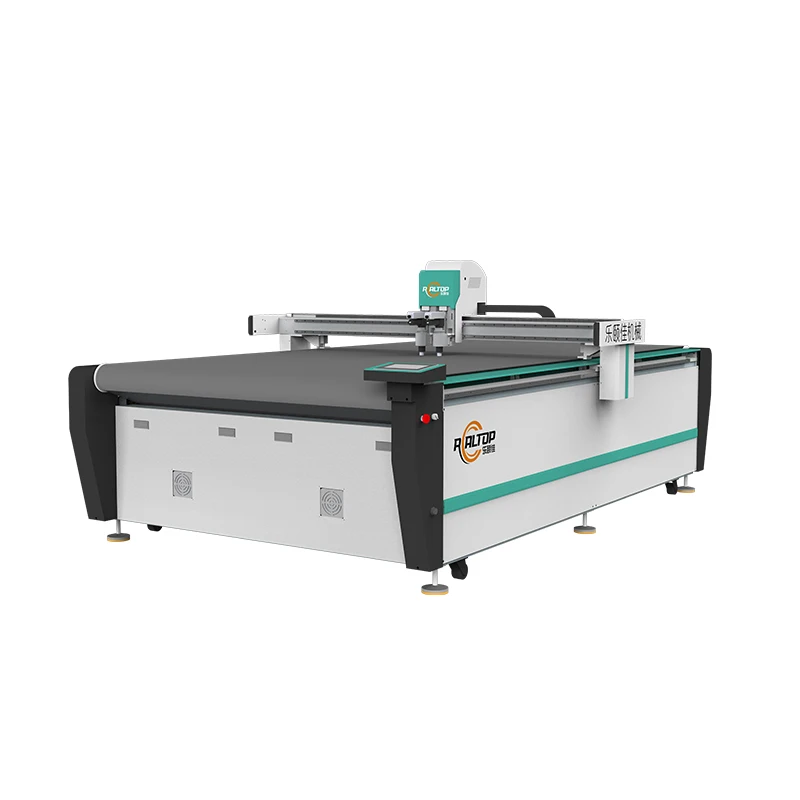
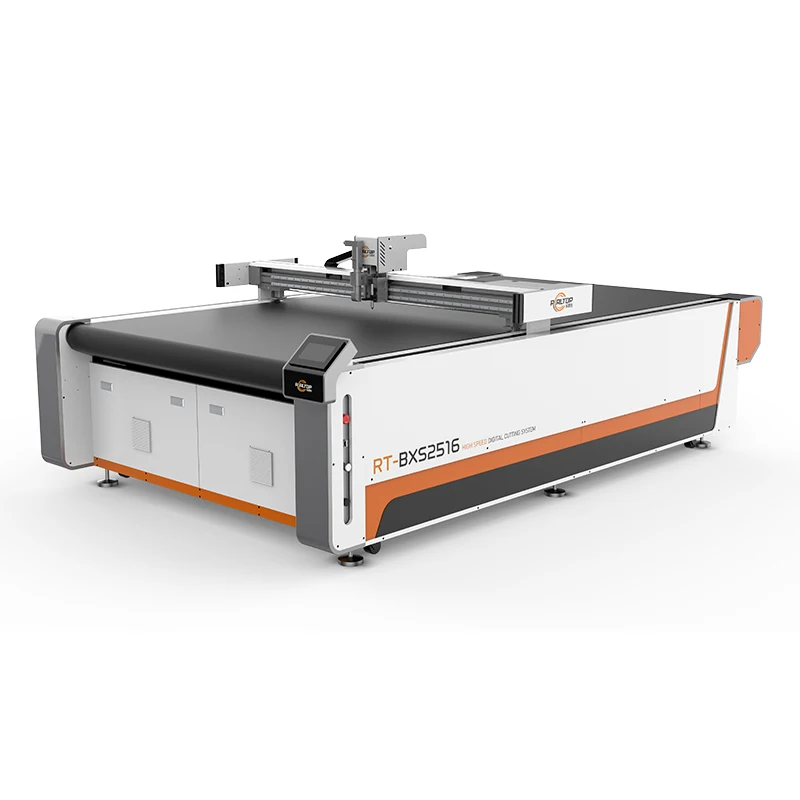
| Model | RT-D2516/RT-S2516 |
| Product Type | CNC Oscillating Knife Leather Cutting Machine |
| Working Area | 1600×2500 mm |
| Machine Size | 3450×2300×1250 mm |
| Rated Power | 9 kW |
| Voltage | 380V±10% (configurable for target market) |
| Vacuum Pump Power | 7.5 kW |
| Working Table | Magnesium-aluminum alloy, PVDF powder sprayed, anodic & hard oxidation treated |
| Multifunctional Tool Head | Swiss imported knife; options include oscillating, pneumatic, high-power vibrating, circular, V-cutting, drag knife, creasing wheel, punching |
| Cutting Thickness | 20–80 mm (basis not stated in source — confirm material type and density) |
| Translational Velocity | 800–1200 mm/s |
| Repeated Accuracy | ≤0.1 mm |
| Transmission System | Digital servo motor, linear guide, synchronous belt, ball screw |
| Servo Motor Brand | Delta (Panasonic optional) |
| Safety Devices | Infrared sensor auto-pause, beam anti-collision stop, emergency stop with in-situ resume |
| Visual Positioning Options | Small CCD camera mark-point, panoramic camera recognition, projection positioning |
| Instruction System | HP-GL compatible format |
| Feeding System | Germany imported conveyor belt, auto feeding |
| Linear Guide | Taiwan Hiwin rail |
| Language Options | English, Russian, Italian, Chinese; special languages customizable |
| Warranty | 1 year (domestic and overseas) |
| Assembly State | Fully assembled |
| Certification | CE (confirm per order) |
Application Suitability
| Application | Material or Output |
|---|---|
| Shoe upper and insole production | Genuine leather, synthetic leather, sponge composite leather |
| Bag and leather goods manufacturing | Full-grain leather, PU leather, PVC with fabric backing |
| Automotive interior trim cutting | Composite leather, sponge-backed materials, soft trim panels |
| Garment pattern cutting | Flexible garment materials, soft shell textiles, layered fabrics |
| Home furnishing and upholstery | Silicon, rubber sheets, soft glass, padded composites |
Why Voltage Confirmation Must Precede the Purchase Order
Specifying a CNC leather cutting machine manufacturer without locking electrical standards first creates avoidable downtime at commissioning.
A batch of oscillating knife machines shipped to a Latin American workshop arrived configured for 50 Hz operation while the facility ran on 60 Hz mains. The spindle motor oversped immediately, producing ragged edges on synthetic leather and forcing a three-week delay while variable frequency drives were sourced locally [NEED_CITE: voltage and frequency standards by export market]. That delay cost the buyer more than any price negotiation could have saved. Electrical mismatch remains one of the most common installation failures in cross-border machinery trade, yet it is entirely preventable when voltage, frequency, plug type, and control panel language are confirmed before the machine enters production.
Who Builds the Machine Matters at the Cutting Edge
Realtop operates as both design house and core factory, meaning the engineering team that specifies the tool head configuration for your leather type is the same team overseeing assembly on the floor. When a CNC leather cutting machine manufacturer controls the full build chain, field feedback loops back into design revisions faster than when a trading company intermediates the transaction. The RT-D2516/RT-S2516 frame, motion components, and vacuum table are produced and tested under one roof before crating.
Build Quality You Can Trace to the Assembly Bay
The magnesium-aluminum alloy table surface undergoes PVDF powder coating followed by anodic and hard oxidation treatment, delivering flatness that holds tolerance across the full 1600×2500 mm working area. Taiwan Hiwin linear guides and imported ball screws maintain the ≤0.1 mm repeated accuracy through continuous production shifts. Delta servo motors carry an IP67 rating and feature real-time automatic gain adjustment with vibration suppression, keeping the knife path stable when cutting dense composite leather [NEED_CITE: IP67 environmental protection rating for industrial servo motors]. This component-level traceability is what separates a factory-built machine from one assembled from unverified sub-assemblies.
Decoding the Specifications That Actually Affect Your Output
The multifunctional tool head accepts Swiss imported knives and supports vibration full cutting, half cutting, and cursor location — but the critical decision is which tool head option matches your material. Oscillating knives slice cleanly through genuine leather up to the stated thickness range, while pneumatic knives handle thicker sponge composites without crushing the core. The 7.5 kW vacuum pump paired with the treated magnesium-aluminum table generates uniform suction across the bed, preventing small leather pieces from lifting during high-speed contour cuts. Translational velocity of 800–1200 mm/s is meaningful only when the vacuum hold-down keeps the material stationary; without adequate zoned suction, speed produces mis-cut parts rather than throughput. The HP-GL compatible instruction system ensures compatibility with standard pattern-making software used in footwear and garment workshops.
The Hidden Cost of Skipping Configuration Verification
Buyers who specify working area alone and defer tool head selection often discover mid-production that the chosen knife cannot handle their material density, producing crushed foam cores or frayed synthetic leather edges. Vacuum table zoning that is too coarse for small pattern pieces causes lift and mis-cuts, wasting hide material that is already expensive per square meter. When CCD contour recognition is promised but not validated at production speed, printed registration marks drift out of tolerance, forcing operators to slow the machine and lose the throughput they originally purchased for [NEED_CITE: common causes of CNC cutting rejection in leather workshops]. These configuration gaps surface only after the machine is installed and the buyer’s production schedule is already committed.
Why Sourcing Directly from the Factory Floor Pays Off
Realtop’s in-house design team covers both knife and laser cutting technologies, so the recommendation is based on your material rather than limited to whatever single technology a reseller happens to stock. Tool head and table configuration are specified per material type and production volume before the order is confirmed. CCD camera positioning options — small mark-point, panoramic recognition, or projection — are matched to your workflow and validated during factory testing. Software compatibility with your existing HP-GL or nesting files is confirmed before the machine ships. Sample cutting on your own leather or composite material provides a physical record that the configuration works before you commit capital [NEED_CITE: best practices for pre-shipment sample verification in machinery procurement].
Documentation & Verification
- Machine specification sheet listing tool head and table configuration matched to your leather type
- Electrical schematic with voltage, frequency, and plug type confirmed for your local grid
- Factory test record documenting cutting performance on your material sample before dispatch
- Software licence and file format compatibility note covering HP-GL and your nesting workflow
- Operation and maintenance manual in your selected control language with spare parts list
Installation, Commissioning & Support
- Fully assembled RT-D2516/RT-S2516 ships ready for placement; verify workshop floor load capacity for the 3450×2300 mm footprint
- Dedicated 380V±10% circuit required; confirm local voltage and frequency before electrical hookup
- 9 kW rated power plus 7.5 kW vacuum pump demand separate breaker sizing at the distribution panel
- First-run commissioning includes servo tuning, vacuum zoning calibration, and knife depth setting for your material
- Operator training covers tool head changeover, CCD positioning setup, and HP-GL file import procedures
- One-year warranty covers domestic and overseas support with consumable knife and belt spare parts identified
What to Include in Your Inquiry
Provide your leather or composite material type, typical thickness range, and maximum sheet dimensions so the tool head and vacuum table can be specified accurately. Confirm your facility voltage, frequency, and preferred control panel language to avoid electrical rework after arrival. If you run existing nesting or pattern software, share a sample file so HP-GL compatibility is verified before the RT-D2516/RT-S2516 enters production.
Frequently Asked Questions
Q: How is cutting thickness verified for my specific leather material?
A: The 20–80 mm range is published without a stated material density basis. Before your order is finalized, we run sample cuts on your actual leather or composite material at your required thickness and document the results in a cutting report. This confirms which tool head option and knife amplitude setting produce clean edges without crushing or fraying.
Q: How do I choose the right tool head for my leather type?
A: Genuine leather, synthetic PU, and sponge composite materials each respond differently to knife action. Oscillating knives suit most genuine and synthetic leathers, while pneumatic or high-power vibrating knives handle thicker composites. We specify the tool head based on the sample material you send and confirm the choice during factory testing.
Q: Is CCD camera positioning validated at full production speed?
A: CCD options include small mark-point, panoramic recognition, and projection positioning. During the factory test, we run your printed or marked material at production translational velocity and document whether the camera tracks registration marks within tolerance throughout the full cutting cycle.
Q: What electrical standards will be configured before shipment?
A: Voltage, frequency, plug type, and control panel language are confirmed during the order specification stage. An electrical schematic reflecting your local grid standard is included in the documentation package, and the machine is wired and tested at those parameters before crating.
Q: Can I send my own material for test cutting before committing?
A: Yes. Send a sample of your leather, synthetic, or composite material with your typical sheet dimensions. We run it on the RT-D2516/RT-S2516 with the proposed tool head configuration, document edge quality and cutting speed, and share the sample cutting report before you approve the order.
You may also like







商品评价
Clear filtersThere are no reviews yet.